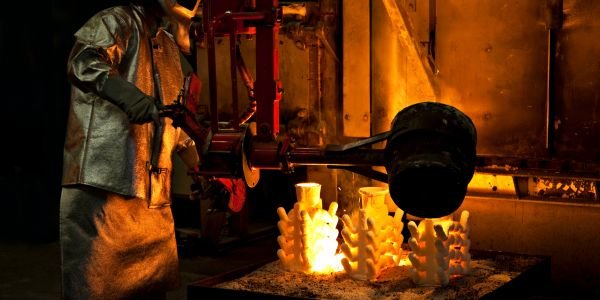
Casting is a manufacturing process in which molten metal is poured into a mould cavity shaped like the part, allowed to solidify, and then removed and cleaned. The main foundry steps are pattern making, moulding (with cores if needed), melting, pouring through a gating system, solidification, shake-out and fettling, and inspection. Casting is often the cheapest way to make complex shapes with internal cavities, such as engine blocks, pump bodies and machine beds.
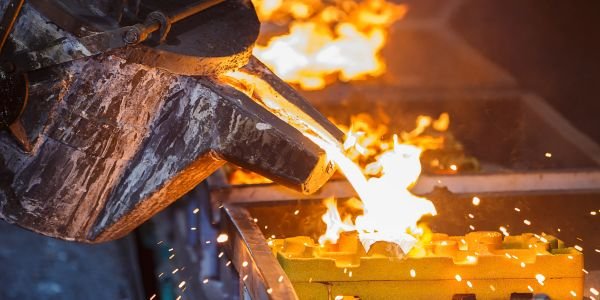
Casting steps in a foundry
The sequence below is for sand casting, the most common foundry process.
1. Pattern making (with allowances)
A pattern is a replica of the part, made in wood, metal, plastic or wax, used to form the mould cavity. It is deliberately oversized by these allowances:
| Allowance | Why it is needed | Typical value |
|---|---|---|
| Shrinkage (contraction) | Metal contracts as the solid casting cools to room temperature | Grey cast iron 7 to 10.5 mm/m (about 1%), steel about 20 mm/m (2%), aluminium alloys 13 to 16 mm/m, brass about 14 mm/m |
| Draft | A slight taper on vertical faces lets the pattern come out of the sand without breaking the mould | About 1 to 3 degrees on external faces, more on internal faces |
| Machining (finish) | Extra metal on surfaces that will be machined, to remove scale and surface defects | A few mm, more for large castings and ferrous metals |
| Distortion (camber) | Long, thin or U-shaped castings warp as they cool; the pattern is bent the opposite way | Decided by experience for each shape |
| Shake (rapping) | Rapping the pattern to loosen it enlarges the cavity slightly | Negative allowance, often ignored for small parts |
2. Moulding
Sand is packed around the pattern in a two-part box called a flask: the upper half is the cope and the lower half the drag. The pattern is then removed, leaving the cavity. Green sand, the everyday moulding material, is roughly 88% silica sand, 9% clay (bentonite) and 3% water. Good moulding sand needs:
- Permeability: lets steam and gases escape during pouring.
- Green and dry strength: holds its shape when handled and when hit by molten metal.
- Refractoriness: does not fuse at the pouring temperature (around 1,400 °C for cast iron, over 1,550 °C for steel).
- Collapsibility: gives way as the casting shrinks, so the casting does not crack, and breaks up easily at shake-out.
- Flowability: packs into fine pattern details when rammed.
3. Cores
A core is a separate sand shape placed in the mould to form holes and internal passages, such as the water jacket in an engine block. Cores are usually made of sand bonded with resin or oil and baked, so they are stronger than the mould. They sit in core prints (seats) and may need chaplets (small metal supports) to resist the upward buoyancy of the molten metal.
4. Melting
Cast iron is melted in a cupola or induction furnace, steel in induction or electric arc furnaces, and aluminium and copper alloys in crucible or induction furnaces. The metal is heated above its melting point (superheat) so it stays fluid while filling the mould.
5. Gating and risering
The gating system is the set of channels that carries metal into the cavity:
- Pouring basin (cup): receives metal from the ladle and reduces splashing.
- Sprue: the vertical channel, tapered downward so the falling stream does not suck in air.
- Runner: the horizontal channel that distributes metal and traps slag.
- Ingates (gates): the openings from the runner into the cavity.
- Riser (feeder): a reservoir of molten metal that feeds the casting as it shrinks during solidification. It must freeze after the casting, so it is made thicker (a common rule is riser modulus at least 1.2 times the casting modulus).
6. Pouring
Metal is poured from a ladle at a controlled temperature and rate. Too cold and thin sections do not fill; too hot and gas pickup and sand burn-on increase.
7. Solidification
The metal freezes from the mould walls inward. Thin sections freeze first and thick sections last, which is why shrinkage cavities form in the thickest (last-to-freeze) region unless a riser feeds it. Chvorinov’s rule estimates the solidification time (worked example below).
8. Shake-out and fettling
After cooling, the mould is broken (shake-out) and cores knocked out. Fettling then cuts off the sprue, runners and risers, grinds off fins and shot blasts the surface.
9. Inspection
Castings are checked visually and dimensionally, and critical parts by pressure testing, dye penetrant or magnetic particle testing for surface cracks, and radiography or ultrasonic testing for internal porosity and shrinkage.
Worked examples
Example 1: pattern length with machining and shrinkage allowance
A grey cast iron shaft must be 400 mm long after machining. Each end gets a 3 mm machining allowance, and shrinkage is taken as 10 mm/m (1%).
- Casting length needed = 400 + 3 + 3 = 406 mm
- Shrinkage = 406 × 0.010 = 4.06 mm
- Pattern length = 406 + 4.06 = 410.06 mm, about 410.1 mm
Note the order: add the machining allowance first, then apply shrinkage to the whole casting dimension, because the extra metal shrinks too.
Example 2: Chvorinov’s rule, cube vs plate
Chvorinov’s rule: t = B (V/A)2, where t is solidification time, V the casting volume, A its surface area, and B a mould constant that depends on the metal and mould material. V/A is called the casting modulus.
Compare two steel castings of the same volume, 1,000,000 mm3 (1 litre), in the same mould material:
| Shape | Volume V | Surface area A | Modulus V/A | (V/A)2 |
|---|---|---|---|---|
| Cube, 100 × 100 × 100 mm | 1,000,000 mm3 | 6 × 1002 = 60,000 mm2 | 16.67 mm | 277.8 mm2 |
| Plate, 200 × 200 × 25 mm | 1,000,000 mm3 | 2(200 × 200) + 4(200 × 25) = 100,000 mm2 | 10.00 mm | 100.0 mm2 |
Ratio of times = 100.0 / 277.8 = 0.36. The plate solidifies in about 36% of the time the cube takes. If the cube needs 5.0 minutes, the plate needs about 1.8 minutes. This is why a riser, which must freeze last, is made compact rather than flat.
Types of casting processes
| Process | Mould | Typical surface finish (Ra) | Typical tolerance | Production volume | Common materials and parts |
|---|---|---|---|---|---|
| Sand casting | Expendable sand mould | 5 to 25 µm | Coarse, about ±1 to ±3 mm depending on size | One-off to high | Cast iron, steel, aluminium, bronze: engine blocks, pump casings, machine beds |
| Shell moulding | Thin resin-bonded sand shell | 1 to 3 µm | About ±0.25 to ±0.5 mm | Medium to high | Iron, steel: crankshafts, camshafts, small valve bodies |
| Investment (lost wax) | Ceramic shell around a wax pattern | 1 to 3 µm | Fine, about ±0.1 to ±0.25 mm | Low to medium | Steels, superalloys: turbine blades, surgical implants, jewellery |
| Gravity die (permanent mould) | Reusable metal mould, metal poured under gravity | 2 to 6 µm | About ±0.3 to ±0.5 mm | Medium to high | Aluminium, copper alloys: pistons, cylinder heads, wheels |
| Pressure die casting | Hardened steel die, metal injected under high pressure | 1 to 2 µm | Fine, about ±0.05 to ±0.2 mm | Very high | Zinc, aluminium, magnesium: gearbox housings, carburettor bodies, laptop frames |
| Centrifugal casting | Rotating mould, metal flung against the wall | 2 to 10 µm | Medium on outer diameter | Medium to high | Cast iron, steel, bronze: pipes, cylinder liners, bushes |
| Continuous casting | Water-cooled open-ended mould | Not a finished part | Section size only | Very high (steel plants) | Steel, copper, aluminium: slabs, billets and blooms for rolling |
Values are typical textbook ranges; the real figure depends on part size, alloy and foundry practice. Research on sand casting parameters is summarised in this ScienceDirect paper on sand casting.
Common casting defects: cause and remedy
| Defect | What it looks like | Main cause | Remedy |
|---|---|---|---|
| Blowhole | Smooth round cavity near the surface | Gas from moist sand or cores trapped in the metal; low permeability | Control sand moisture, improve venting and permeability, dry cores |
| Gas porosity | Many small scattered holes | Dissolved hydrogen or nitrogen coming out as the metal solidifies | Degas the melt, use dry charge materials, avoid excessive superheat |
| Shrinkage cavity | Rough, jagged cavity in thick sections | Last-to-freeze region not fed with liquid metal | Add or enlarge risers, use chills, design uniform sections |
| Cold shut | Line or seam where two metal streams met but did not fuse | Metal too cold, slow pouring, poor gating | Raise pouring temperature, pour faster, add ingates |
| Misrun | Casting incomplete, thin section not filled | Metal froze before filling the cavity; low fluidity or thin walls | Higher pouring temperature, thicker sections, better gating |
| Hot tear | Irregular crack formed at high temperature | Mould or core resists contraction; sharp corners | Improve collapsibility, add fillets, avoid abrupt section changes |
| Inclusions | Sand or slag particles in the metal | Eroded mould sand, slag carried in from the ladle | Stronger mould, skim slag, use a slag trap or filter in the runner |
Advantages and limitations of casting
| Advantages | Limitations |
|---|---|
| Makes complex shapes and internal cavities in one piece | Sand castings have rough surfaces and loose tolerances, so machining is often needed |
| Almost any metal can be cast, including ones hard to forge (grey iron) | Cast structures usually have lower strength and toughness than forged parts |
| Size range from grams to hundreds of tonnes | Defects such as porosity and shrinkage need inspection |
| Low tooling cost for sand casting; very low part cost for die casting at volume | Die casting tooling is expensive and limited to low-melting alloys |
Applications of casting in manufacturing
Automobiles use more castings than almost any other product: cylinder blocks and heads, pistons, crankshafts, brake drums and discs, gearbox housings and alloy wheels are all cast. The chassis frame itself is usually pressed and welded steel, but many cast parts such as suspension brackets, axle housings and steering knuckles are mounted on it, and some modern vehicles use large aluminium die castings as structural parts. Read more about chassis frame types and materials.
Other common uses are pipes, pump and valve bodies, machine tool beds (grey iron damps vibration well), turbine blades and railway brake blocks. Metal casting is part of the Manufacturing Processes course in the AICTE model curriculum for B.Tech Mechanical and Production Engineering.
FAQs
What are the main steps of the casting process?
Pattern making, mould making (with cores if needed), melting, pouring through the gating system, solidification, shake-out and fettling, and inspection.
Why is a shrinkage allowance given on a pattern?
Because metal contracts as the casting cools to room temperature. The pattern is made larger, by about 1% for grey cast iron and about 2% for steel, so the finished casting comes out at the right size.
What is the purpose of a riser in casting?
A riser is a reservoir of molten metal that feeds the casting as it shrinks during solidification. It must solidify after the casting, so it is made with a larger volume-to-area ratio than the section it feeds.
Which casting process gives the best surface finish?
Pressure die casting and investment casting give the smoothest surfaces and closest tolerances, around 1 to 3 µm Ra. Sand casting gives the roughest surface.
What is the difference between a pattern and a core?
A pattern forms the outer shape of the casting in the mould and is removed before pouring. A core is a sand shape left in the mould to form holes and internal passages, and is broken out after the casting solidifies.