Annealing is a heat treatment in which a metal is heated to a set temperature, held there (soaked), and then cooled slowly, usually inside the furnace, to make it softer and more ductile, remove internal stress and refine its grain. For steel, full annealing means heating 30-50 °C above the upper critical temperature (A3) and furnace cooling; for cold-worked copper, aluminium or brass it means heating above the recrystallisation temperature so new, strain-free grains replace the deformed ones.
This page takes annealing in depth. For how it fits alongside hardening, tempering and case hardening, start with the heat treatment of steel hub.
Why annealing is done
Annealing is used for four jobs, and a single cycle often does several at once:
- Soften the metal so it machines, presses or draws easily. A fully annealed medium-carbon steel cuts faster and with less tool wear than the same steel as rolled.
- Restore ductility after cold working. Wire drawing, deep drawing and cold rolling harden the metal until it cracks; an anneal between passes lets forming continue.
- Relieve internal stress left by welding, casting, uneven cooling or heavy machining, so the part does not distort or crack later.
- Refine and even out the grain, removing the coarse or uneven structure left by casting or forging and giving a known starting point before hardening.
How annealing works: the three stages
When a metal is cold worked, its crystals fill with dislocations (line defects in the atomic lattice). They tangle and block each other, which is why cold-worked metal is hard and has lost ductility. That tangle also stores energy. Annealing supplies heat so atoms can move and the metal can release that stored energy in three stages.
1. Recovery
At the lowest temperatures, dislocations move short distances and rearrange into low-energy walls, forming small sub-grains inside the old deformed grains (polygonisation). Vacancies and other point defects are removed. The grain shape does not change and hardness falls only a little, but internal stresses drop and electrical conductivity comes back. Stress-relief annealing works in this stage.
2. Recrystallisation
At a higher temperature, completely new grains nucleate where the stored energy is highest, at old grain boundaries and heavily deformed bands. These new grains are equiaxed (roughly equal in all directions) and almost free of dislocations. They grow and consume the deformed grains until the whole volume is new. Dislocation density falls sharply, so hardness and strength drop and ductility returns to roughly the pre-cold-work level. This is the stage that process annealing aims for.
3. Grain growth
If heating continues after recrystallisation is complete, larger grains grow at the expense of smaller ones to reduce the total grain-boundary area. The metal gets softer still, but strength and toughness fall, and sheet can show a rough “orange peel” surface when formed. Grain growth is usually something to limit, by keeping the temperature and soak time no higher than needed.
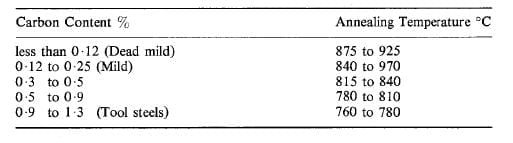
The table above, from a classic workshop text, lists annealing temperatures by carbon content. The pattern matches the iron-carbon diagram: the more carbon, the lower the temperature, down to 760-780 °C for tool steels (just above A1). The “840 to 970” figure in the mild steel row is probably a misprint for 840 to 870, given the rows either side.
Recrystallisation temperature
The recrystallisation temperature is the temperature at which a cold-worked metal fully recrystallises in a practical time, usually taken as about one hour. It is not a fixed property like the melting point. As a rule of thumb it is about 0.3 to 0.5 of the absolute melting temperature (in kelvin): about 0.3-0.4 Tm for pure metals and about 0.5 Tm for alloys.
It comes down when:
- the amount of prior cold work is larger (more stored energy, more nuclei);
- the metal is purer (alloying and impurity atoms pin grain boundaries);
- the original grain size is finer (more boundary sites for new grains);
- the holding time is longer.
Below a small critical amount of cold work, typically a few percent, the metal does not recrystallise at all, and just above it only a few nuclei form, which can give very coarse grains.
Worked example: recrystallisation temperature of copper and aluminium
Copper, melting point 1085 °C.
- Convert to kelvin: Tm = 1085 + 273 = 1358 K.
- 0.3 Tm = 0.3 × 1358 = 407 K = 134 °C.
- 0.5 Tm = 0.5 × 1358 = 679 K = 406 °C.
- So cold-worked copper recrystallises somewhere between about 134 °C and 406 °C. Pure copper sits in the lower part (0.3-0.4 Tm gives 134-270 °C).
Aluminium, melting point 660 °C.
- Tm = 660 + 273 = 933 K.
- 0.3 Tm = 0.3 × 933 = 280 K = 7 °C.
- 0.5 Tm = 0.5 × 933 = 467 K = 194 °C.
- Range: about 7 °C to 194 °C. Pure aluminium can recover and soften at quite low temperatures, which is one reason aluminium alloys, not pure aluminium, are used where strength matters.
The same rule for iron (Tm 1538 °C = 1811 K) gives 0.4-0.5 Tm = 451-632 °C, which is why process annealing of low-carbon steel is done at 550-650 °C. A common student mistake is to multiply the melting point in °C by 0.4. Always convert to kelvin first, then convert back.
Types of annealing for steel
The temperatures below are the same ones used on the heat treatment of steel page. A1 is 727 °C; A3 falls from 912 °C at zero carbon to 727 °C at about 0.77 percent carbon.
| Type | Temperature | Cooling | Used for |
|---|---|---|---|
| Full annealing | A3 + 30-50 °C (hypoeutectoid); A1 + 30-50 °C (hypereutectoid) | Very slow, in the switched-off furnace | Maximum softness in castings, forgings, bar before machining |
| Process (subcritical) annealing | 550-650 °C, below A1 | Air or furnace | Restoring ductility to cold-worked low-carbon sheet and wire between stages |
| Spheroidise annealing | Just below A1, about 700 °C, long hold (or cycling around A1) | Slow | High-carbon and bearing steels before machining or cold heading |
| Stress-relief annealing | About 550-650 °C | Slow, to avoid new stress | Welded fabrications, heavily machined parts, castings |
| Isothermal annealing | Austenitise as for full annealing, then cool quickly to a hold a little below A1 until transformation is complete | Air after the hold | Alloy steels where a full furnace cool would take too long |
Full annealing
A hypoeutectoid steel is heated just above A3 so it becomes fully austenite, soaked, and cooled slowly in the furnace. The austenite transforms to coarse pearlite and ferrite, the softest normal structure. Hypereutectoid steels are heated only above A1: heating them above Acm and slow cooling would leave a brittle network of cementite around the grain boundaries.
Example: for a 0.4 percent carbon steel, A3 is about 800 °C, so full annealing is at about 830-850 °C. For a 1.0 percent carbon tool steel it is 727 + 30 to 50 = about 757-777 °C, in line with the 760-780 °C row in the table above.
Process annealing
Cold-rolled sheet and drawn wire in low-carbon steel harden with each pass. Heating to 550-650 °C, below A1, recrystallises the ferrite without forming austenite. It is cheaper than full annealing and gives less scaling. Batch (box) annealing of cold-rolled coils is this process.
Spheroidise annealing
Holding high-carbon steel for many hours just under A1 lets the cementite plates in pearlite ball up into small spheres in a ferrite matrix. This gives the softest, most machinable and most formable condition a high-carbon steel can have, and is standard for bearing steels such as EN31 before machining.
Stress-relief annealing works only in the recovery stage: the structure hardly changes, but residual stress from welding or machining falls to a low level, so heavy welded frames and pressure vessels are often stress relieved before final machining. Isothermal annealing replaces the long furnace cool with a hold just below A1 until the austenite has fully turned to pearlite, giving a uniform structure in less furnace time.
The annealing furnace cycle
- Heat at a controlled rate. Large or complex parts are heated slowly or in steps so the surface and core stay close in temperature.
- Soak at temperature so the whole section reaches it and transforms. The common shop rule is about one hour per 25 mm of thickness. Worked example: a 75 mm thick die block needs 75 / 25 = 3 hours at temperature, counted from the time the centre, not the furnace, reaches it.
- Cool slowly. For full annealing the furnace is switched off with the door closed so the steel cools through the transformation range over many hours; once it is well below A1 it can be taken out and air cooled. The exact rate comes from the steel supplier’s data sheet.
To stop scaling and carbon loss, annealing is done in a protective gas atmosphere, a vacuum furnace, or with parts packed in cast-iron chips or sealed boxes. Bright annealing of cold-rolled strip and stainless tube uses a reducing gas such as hydrogen-nitrogen so the surface comes out clean.
Annealing non-ferrous metals
Copper, aluminium and their alloys have no phase change like steel’s ferrite-to-austenite, so annealing them is purely a recovery and recrystallisation treatment. The cooling rate matters much less.
- Copper: heated above its recrystallisation temperature and can then be cooled in air or even quenched in water, which also loosens surface oxide. Annealed copper wire is the soft wire used for house wiring and windings.
- Aluminium alloys: the fully annealed condition is called the O temper (for example 1100-O or 6061-O). Heat-treatable alloys such as 6061 and 2024 need a controlled slow cool after annealing, or they partly harden again. Take the temperature and cooling rate from the alloy data sheet.
- Brass: fully annealed between deep-drawing stages, for example in cartridge-case and tube making. Cold-worked brass also gets a low-temperature stress-relief anneal, typically a few hundred degrees Celsius, to prevent season cracking (stress-corrosion cracking in moist, ammonia-bearing air).
Annealing glass
Glass is annealed for a different reason: to remove stress, not to soften it. After forming, the outside of a glass article cools faster than the inside and locks in stress. It is reheated to its annealing point (the temperature where its viscosity is about 1013 poise, roughly 454-482 °C for most common glasses), held so the stress relaxes, then cooled slowly through the strain point (about 1014.5 poise), below which it can no longer flow. The long oven used for this is called a lehr. Poorly annealed glass can crack from a small temperature change or even break on its own.
Annealing vs normalising vs tempering
| Feature | Annealing (full) | Normalising | Tempering |
|---|---|---|---|
| Starting condition | Any: cast, forged, cold worked | Cast, forged or rolled | Hardened (quenched) steel only |
| Temperature | A3 + 30-50 °C (A1 + 30-50 °C for hypereutectoid) | A3 or Acm + 30-50 °C | 150-650 °C, always below A1 |
| Cooling | In the furnace, very slow | In still air | Usually air |
| Structure | Coarse pearlite + ferrite | Fine pearlite + ferrite | Tempered martensite |
| Hardness and strength | Lowest | Somewhat higher | High, set by tempering temperature |
| Main aim | Softness, machinability, ductility | Uniform fine grain, moderate strength | Toughness after hardening |
| Furnace time | Longest | Short | Short to moderate |
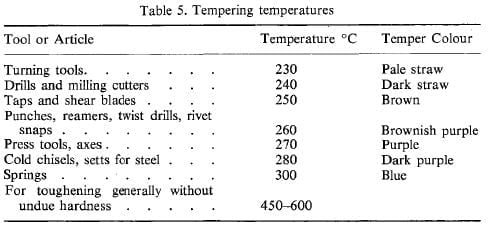
The image above is a tempering table, not an annealing one. It shows how different the two treatments are: tempering of hardened tools happens at 230-300 °C, identified in older shops by the oxide colour (pale straw to blue), while annealing of the same steels needs 760 °C or more.
Effects of annealing on properties
- Hardness, yield strength and tensile strength: go down.
- Ductility (percent elongation) and formability: go up, often back to the level before cold work.
- Machinability: improves for medium and high-carbon steels. Very low-carbon steels can become too soft and “gummy” when fully annealed, so they are often normalised instead.
- Residual stress: reduced to a low level.
- Electrical conductivity: rises in cold-worked copper and aluminium, which is why conductor wire is annealed.
- Young’s modulus: practically unchanged. Annealing alters strength, not stiffness.
See mechanical properties of metals for how cold work, grain size and heat treatment move these numbers, and hardness testing for how annealed parts are checked.
Annealing defects and how to avoid them
- Decarburisation: carbon burns out of the surface in an oxidising furnace, leaving a soft skin that later will not harden. Use a protective atmosphere, vacuum or pack annealing, or leave a machining allowance.
- Scaling (oxidation): loses metal and spoils the finish. Same remedies as above.
- Grain coarsening: from too high a temperature or too long a soak, giving low toughness and orange peel on formed sheet. Keep to A3 + 30-50 °C and the one-hour-per-25 mm rule; a coarse-grained part can be rescued by normalising.
- Abnormal grain growth after light cold work: parts with only a few percent strain can grow a few very large grains. Avoid annealing parts that have just the critical amount of deformation.
- Overheating and burning: close to the melting range, grain boundaries oxidise or melt. Burnt steel cannot be recovered and is scrapped.
- Incomplete annealing: too short a soak or too low a temperature leaves hard spots; check hardness at several points.
- Cementite network in hypereutectoid steel: from heating above Acm and cooling slowly. Anneal these steels from just above A1.
Reference data for annealing cycles of specific alloys is published by ASM International in its heat treating handbooks. For how cold work builds up in the first place, read hot working and cold working of steel.
FAQs
What is annealing in simple words?
Annealing is heating a metal to a set temperature, holding it there, and cooling it slowly so it becomes softer, more ductile and free of internal stress. It undoes the hardening caused by cold working, welding or uneven cooling.
What are the three stages of annealing?
Recovery, where dislocations rearrange and internal stresses fall; recrystallisation, where new strain-free grains replace the deformed ones and the metal softens; and grain growth, where the new grains coarsen if heating continues.
At what temperature is steel annealed?
Full annealing of hypoeutectoid steel is done 30-50 °C above A3, about 830-850 °C for 0.4 percent carbon steel, and of hypereutectoid steel 30-50 °C above A1 (727 °C). Process and stress-relief annealing use about 550-650 °C.
How is recrystallisation temperature calculated?
As a rule of thumb it is 0.3 to 0.5 times the melting temperature in kelvin. For copper (1358 K) this gives about 134-406 °C. The real value falls with more cold work, higher purity and longer holding time.
What is the difference between annealing and tempering?
Annealing softens any metal by heating and slow cooling, and for steel usually goes above the critical temperature. Tempering is done only on hardened steel, always below A1 (150-650 °C), to trade some hardness for toughness.