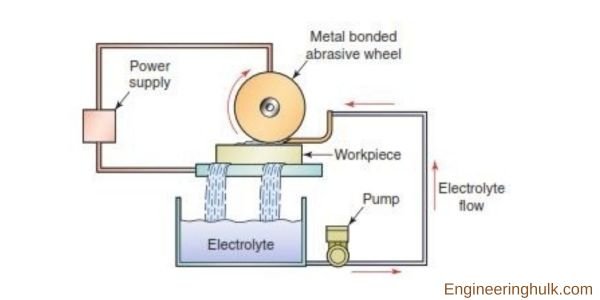
Electrochemical grinding (ECG), also called electrolytic grinding, is a hybrid process in which a rotating, electrically conductive abrasive wheel (the cathode) removes metal from a workpiece (the anode) mainly by anodic dissolution in a flowing electrolyte, while the abrasive grains remove a small share mechanically and scrape away the oxide film. The workpiece must conduct electricity. Because most of the metal is dissolved rather than cut, ECG leaves burr-free edges, adds almost no heat and puts very little force on the part, which is why it is used for carbide tools, thin tubes, surgical needles and other medical components.
What is electrochemical grinding?
ECG combines electrochemical machining (ECM), which dissolves metal atom by atom with direct current, with conventional grinding. The machine looks like a surface or cut-off grinder, but the wheel barely touches the metal: the protruding abrasive grains act as insulating spacers that hold a tiny gap between the metal bond of the wheel and the work.
How much of the metal is removed electrochemically? Textbooks usually quote about 90% by electrolysis and 10% by abrasion, and some give 95% or more. Treat that as a typical figure, not a rule. Glebar, which builds ECG machines, points out that the split changes with the settings: at around 2 V the cut is mostly abrasive, while at around 15 V it is mostly electrochemical.
Construction of an electrochemical grinding machine
An electrochemical grinding machine looks much like a conventional surface or cut-off grinder, with an electrical and electrolyte system added. The main parts are:
| Part | What it is and what it does |
|---|---|
| Grinding wheel (cathode) | Metal-bonded wheel, with a bond of copper, brass or nickel holding diamond, CBN or aluminium oxide grains. The bond conducts current; the grains are insulators that stick out slightly and keep the gap. |
| Workpiece (anode) | Any electrically conductive metal: tungsten carbide, hardened tool steel, stainless steel, nickel and cobalt alloys. |
| DC power supply | Low voltage, high current. Glebar gives a typical range of 4 to 15 V, with 7 to 10 V most common; supplies are made in sizes such as 300, 600 and 1000 A. |
| Brush or slip ring | Carries current into the rotating spindle and wheel. |
| Electrolyte system | Tank, pump, filter and nozzle. The nozzle feeds electrolyte into the gap where the wheel meets the work. |
| Electrolyte | Water-based salt solution, most often sodium nitrate (NaNO3); sodium chloride, sodium nitrite and other salts are also used. A common strength is about 20% by weight. |
| Machine body and table | Spindle, feed slide and an insulated work-holding fixture, so current only flows through the wheel-to-work gap. |
Sodium nitrate is popular because it is cheap and less corrosive to the machine than sodium chloride.
Working of electrochemical grinding, step by step
- Set up the circuit. The workpiece is connected to the positive terminal and the wheel to the negative terminal of the DC supply.
- Start the wheel and electrolyte. The wheel rotates at a surface speed of roughly 1200 to 2000 m/min, and electrolyte is pumped into the zone where wheel and work meet.
- Hold the gap. The abrasive grains rest on the work and keep the metal bond a small distance away. Sources give a gap of about 0.025 mm, and up to about 0.05 mm.
- Dissolve the anode. Current flows through the electrolyte in the gap. Metal atoms on the workpiece surface lose electrons and go into solution as ions (for iron, Fe goes to Fe2+). Hydrogen gas is given off at the wheel; no metal plates onto it.
- Scrape off the film. Dissolution leaves a thin oxide film that would slow the reaction. The abrasive grains wipe it away, exposing fresh metal, and also remove a small amount of metal themselves.
- Flush the products. The electrolyte carries away the metal hydroxide sludge, gas bubbles and heat.
- Feed the work. The table or wheel is fed at a rate that matches the dissolution rate. Feed too fast and the grains take more of the load, so wheel wear and heat rise; feed too slowly and time is wasted.
Material removal rate from Faraday’s law
The electrochemical part of the removal follows Faraday’s law of electrolysis. The volume removed per second is:
MRR = (I × A) / (Z × F × ρ)
- I = current (A)
- A = atomic mass of the workpiece metal (g/mol)
- Z = valency of dissolution (charge on the ion formed)
- F = Faraday’s constant = 96,485 C/mol
- ρ = density of the workpiece (g/cm3)
This gives MRR in cm3/s and assumes 100% current efficiency. Real efficiency is lower, and the small abrasive share adds a little on top, so treat the result as an estimate.
Worked example: grinding iron at 300 A
An iron workpiece is ground at a current of 300 A. Take A = 55.85 g/mol, ρ = 7.87 g/cm3 and assume iron dissolves as Fe2+, so Z = 2.
- Mass removed per second = I × A / (Z × F) = 300 × 55.85 / (2 × 96,485) = 0.0868 g/s, or about 5.2 g/min.
- Volume removed per second = 0.0868 / 7.87 = 0.0110 cm3/s = 11.0 mm3/s.
- Per minute: 11.0 × 60 = about 660 mm3/min.
If the wheel and work are in contact over an area of 200 mm2 (say 20 mm by 10 mm), the matching feed rate is 11.0 / 200 = 0.055 mm/s, or about 3.3 mm/min.
The valency matters. If you assume iron dissolves as Fe3+ (Z = 3), the same current removes only about 440 mm3/min. For nickel (A = 58.69 g/mol, Z = 2, ρ = 8.91 g/cm3) at 300 A, the answer is about 10.2 mm3/s, or 615 mm3/min. Always state your valency assumption in an exam answer.
Process parameters and their effects
| Parameter | Effect of increasing it |
|---|---|
| Current (current density) | MRR rises in direct proportion (Faraday’s law). Too high a density can cause sparking and pitting. |
| Voltage | Raises current and shifts the removal towards the electrochemical side. Too high and the gap sparks over, like EDM, which damages the wheel and surface. |
| Electrolyte concentration and flow | Higher conductivity and steady flow give more current and better flushing. Poor flow lets sludge and gas build up and causes uneven removal. |
| Wheel speed | Drags more electrolyte into the gap and improves finish. |
| Feed rate | Must match the dissolution rate. Too fast shifts the work onto the abrasive grains, raising wheel wear, heat and burrs. |
| Grit size | Sets the gap size, because the grains are the spacers. Finer grit gives a smaller gap and a finer finish. |
Advantages of electrochemical grinding
- Burr-free edges: dissolution does not push metal over an edge, so parts often need no deburring.
- Low heat and stress: no burn marks, heat-affected zone or grinding cracks. Thin walls and heat-sensitive parts do not distort.
- Hardness does not matter much: removal depends on conductivity and chemistry, so carbides and hardened alloys cut as readily as softer steels.
- Long wheel life: the grains do little cutting. Glebar quotes G-ratios of about 10 to 15 for aluminium oxide wheels and up to about 100 for super-abrasive wheels.
- Low cutting forces: fragile parts such as honeycomb and thin-wall tube do not collapse or bend.
Limitations
- Works only on electrically conductive materials; not on ceramics, glass or plastics.
- Higher capital cost than a conventional grinder: power supply, electrolyte handling, filtration and corrosion-resistant construction.
- The electrolyte is corrosive to the machine and the part, so parts must be rinsed and machines protected.
- Sludge contains dissolved metals (for carbide, cobalt and tungsten compounds) and must be disposed of properly.
- Sharp inside corners are hard to hold, because dissolution rounds edges slightly.
Applications of electrochemical grinding
- Carbide tools: sharpening and regrinding tungsten-carbide cutting tools and inserts, the classic ECG job.
- Medical components: pointing hypodermic needles, surgical needles, trocars and biopsy needles, and cutting thin-wall stainless steel tubes. Conventional grinding leaves burrs that must be blasted or electropolished off, which dulls the tip; ECG avoids most of those burrs.
- Tube and wire cut-off: burr-free cutting of small tubes and wire, from medical tubing to small tubes for aircraft engines.
- Aerospace: honeycomb seals and turbine airfoils, where the material is thin, fragile and heat sensitive.
ECG vs conventional grinding vs ECM
| Feature | Electrochemical grinding (ECG) | Conventional grinding | Electrochemical machining (ECM) |
|---|---|---|---|
| Main removal mechanism | Anodic dissolution plus a small abrasive share | Abrasive cutting only | Anodic dissolution only |
| Tool | Rotating conductive metal-bonded abrasive wheel | Rotating abrasive wheel (vitrified, resin or metal bond) | Shaped cathode tool, no abrasive |
| Tool-work contact | Grains touch lightly; metal bond does not | Full abrasive contact | No contact |
| Workpiece material | Conductive only | Any, including ceramics | Conductive only |
| Effect of hardness | Small | Large: harder work means slower cutting and more wheel wear | None |
| Heat and burrs | Very low heat, burr-free | Heat, possible burns and burrs | No heat, burr-free |
| Typical shapes | Flat, cylindrical, cut-off, tool edges | Flat, cylindrical, profiles | Complex 3D cavities and profiles |
| Typical uses | Carbide tools, needles, thin tubes, honeycomb | General finishing of shafts, bores, flat parts | Turbine blades, dies, deep holes |
For the basics of a plain grinder, see grinder machine working and types. Other non-traditional processes compare as follows: electrical discharge machining (EDM) erodes conductive metal with sparks and leaves a recast layer, while chemical machining dissolves metal through a mask without any current. For an overview of all removal methods, see material removal techniques in manufacturing. Lecture series on unconventional machining are available on NPTEL.
FAQs
What is electrochemical grinding?
Electrochemical grinding is a hybrid machining process in which a conductive abrasive wheel acts as the cathode and the workpiece as the anode in an electrolyte. Most of the metal is dissolved electrochemically, and the abrasive grains remove the rest and scrape off the oxide film.
Is electrolytic grinding the same as electrochemical grinding?
Yes. Electrolytic grinding, electro chemical grinding and ECG all name the same process.
How much material is removed by abrasion in ECG?
Textbooks usually say about 10%, with 90% removed electrochemically. The real split depends on voltage and feed: low voltage makes the cut mostly abrasive, higher voltage makes it mostly electrochemical.
Why is electrochemical grinding used for medical components?
ECG leaves burr-free edges with no heat damage and very low force, so thin stainless steel tubes and needle points stay sharp and undistorted. That makes it a common choice for hypodermic, surgical and biopsy needles and for cutting medical tubing.
Which electrolyte is used in electrochemical grinding?
Sodium nitrate solution is the most common, often at about 20% strength. Sodium chloride, sodium nitrite and other salts are also used.