Hot working is plastic deformation of a metal above its recrystallisation temperature; cold working is deformation below it. The dividing line is the recrystallisation temperature of that metal, not a fixed number of degrees. Hot working (hot rolling, forging, extrusion, piercing) needs less force and refines the grain but leaves scale and loose tolerances. Cold working (cold rolling, drawing, bending, heading, coining) strengthens the metal by strain hardening and gives a bright, accurate surface, at the cost of ductility and higher forces.
The dividing line: recrystallisation temperature
When a metal is deformed, its grains are squashed and filled with dislocations, which makes it harder. Above the recrystallisation temperature, new strain-free grains form almost as fast as the old ones are deformed, so the metal never builds up that hardening. That is hot working. Below it, the hardening stays in the metal. That is cold working.
As a rule of thumb the recrystallisation temperature is about 0.3-0.5 of the melting point in kelvin (the annealing page explains why it shifts with purity, amount of cold work and time). Because it is a fraction of the melting point, “hot” and “cold” mean very different things for different metals.
Worked example: lead, tungsten and steel
- Lead, melting point 327 °C = 600 K. At 0.4 Tm: 0.4 × 600 = 240 K = -33 °C. Squeezing lead at room temperature (about 25 °C) is therefore hot working: it does not work harden, which is why lead pipe and sheet can be bent again and again.
- Tungsten, melting point 3422 °C = 3695 K. At 0.4 Tm: 0.4 × 3695 = 1478 K = about 1205 °C. Working tungsten at 1000 °C, when it is glowing orange, is still cold working.
- Iron and steel, melting point about 1538 °C = 1811 K. At 0.4-0.5 Tm: 724-906 K = about 451-632 °C. In practice steel is hot worked much hotter, in the austenite range, where it is soft and easy to shape; forging of carbon steel is typically started somewhere around 1100-1250 °C.
Warm working sits between the two, roughly 0.3-0.5 Tm for many metals. It needs less force than cold working and gives better accuracy and less scale than hot working, and is used for some precision forgings.
Hot working processes
- Hot rolling: a hot slab, bloom or billet is passed between rotating rolls to reduce its thickness. It produces plate, strip, angles, channels, beams, rails and wire rod. Almost all steel is hot rolled at some stage.
- Forging: the hot metal is hammered or pressed into shape, in open dies (large shafts, rings) or closed dies (crankshafts, connecting rods, spanners). Upset forging thickens one end of a bar, as for bolt heads and shaft flanges.
- Hot extrusion: a hot billet is pushed through a die to make long lengths of constant cross-section, such as tubes and complex sections.
- Piercing: the rotary (Mannesmann) process makes tubes with no welded seam by rolling a hot round billet between two skewed rolls over a pointed plug, which opens a hole along its axis.
- Hot spinning and hot drawing of heavy plate, for pressure-vessel ends and large cylinders.
Hot working breaks up the coarse, porous structure of a cast ingot, closes internal voids, and gives a fine, uniform grain. It also lines up inclusions and grain boundaries into a fibre (flow lines) that follows the shape of the part.
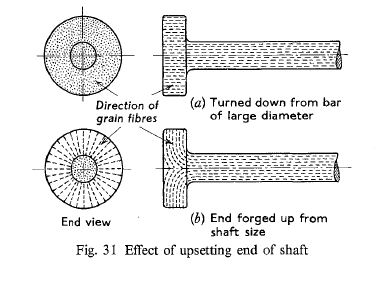
The figure shows why forged parts are stronger than parts machined from bar. In (a), the flange is turned from a large bar, so the grain fibres run straight through and are cut at the corner, a weak spot. In (b), the end is upset forged, and the fibres flow round the flange, following the direction of stress.
Cold working processes
- Cold rolling: pickled hot-rolled strip is rolled at room temperature to a thinner, flatter, brighter sheet with close thickness tolerance.
- Drawing: wire drawing pulls rod through a series of dies of decreasing diameter; tube drawing and bar drawing give bright bar and precision tube.
- Bending and pressing: brake pressing, roll forming, deep drawing of cups, cans and car panels. See sheet metal fabrication for these operations.
- Cold heading: forming the heads of bolts, screws and rivets from wire in a die, at very high production rates.
- Coining: squeezing metal in a closed die so it flows into fine detail on both faces, as on coins and medals.
- Others: cold extrusion, spinning, thread rolling, shot peening.
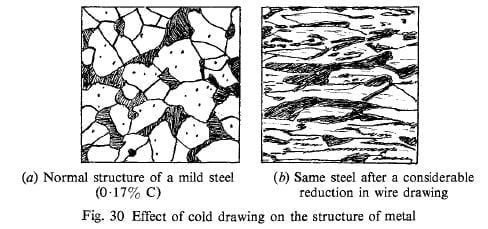
The micrographs show what cold drawing does inside a mild steel wire. The roughly equal-sized grains in (a) are stretched into long, thin grains along the wire in (b). Those distorted grains carry a high density of dislocations, which is where the extra strength comes from.
What is strain hardening?
Strain hardening (work hardening) is the rise in strength and hardness of a metal as it is plastically deformed below its recrystallisation temperature. Plastic flow happens by dislocations sliding through the crystal. Deformation also creates new dislocations, and as their number grows they get in each other’s way and pile up at grain boundaries. More stress is then needed to keep them moving, so yield strength and hardness go up while ductility goes down.
Bend a paper clip back and forth: it gets stiffer to bend just before it snaps. Taken far enough, cold-worked metal cracks, so it is given a process anneal between stages to recrystallise it and restore ductility. Strain hardening is used on purpose too: the hard-drawn temper of copper wire and the H tempers of aluminium sheet are produced this way. For the numbers, see mechanical properties of metals.
Hot working vs cold working: effects table
| Property or factor | Hot working | Cold working |
|---|---|---|
| Temperature | Above recrystallisation temperature | Below recrystallisation temperature (usually room temperature) |
| Strength and hardness | Not increased; no strain hardening | Increased by strain hardening |
| Ductility | Retained or improved | Reduced; may need annealing between stages |
| Grain structure | Fine, equiaxed, recrystallised | Elongated, distorted grains |
| Surface finish | Rough, with oxide scale | Smooth and bright |
| Dimensional accuracy | Lower; the part shrinks as it cools | High, close tolerances |
| Residual stress | Low | Can be high; may need stress relief |
| Force and power needed | Low | High |
| Deformation per pass | Large | Limited before cracking |
| Directional properties | Fibre (flow lines) from elongated inclusions | Stronger along the working direction |
| Tooling and handling | Tools must resist heat; hot metal is harder to handle | Simpler handling; tools take high loads |
Worked examples: percent cold work
The amount of cold work is expressed as the percentage reduction in cross-sectional area:
% cold work = (A0 – Af) / A0 × 100
where A0 is the original area and Af the final area.
Example 1: wire drawn from 5 mm to 4 mm
- A0 = π/4 × 52 = 19.63 mm2
- Af = π/4 × 42 = 12.57 mm2
- % cold work = (19.63 – 12.57) / 19.63 × 100 = 36%
Shortcut: the π/4 cancels, so % cold work = (52 – 42) / 52 × 100 = 9 / 25 × 100 = 36%. Note that the diameter fell by only 20%, but the area fell by 36%. Using the diameter instead of the area is the most common mistake in this calculation.
Example 2: sheet cold rolled from 3 mm to 2 mm
- In rolling, the width of a sheet hardly changes, so the reduction in area equals the reduction in thickness.
- % reduction = (3 – 2) / 3 × 100 = 33.3%
- Volume stays constant in plastic deformation, so the length increases by 3 / 2 = 1.5 times: a 1 m length of 3 mm sheet comes out about 1.5 m long.
Hot-rolled vs cold-rolled steel sheet
This is where the difference is most visible in a steel yard. In India, hot-rolled structural plate and sections are usually bought to IS 2062 (for example grade E250), and cold-rolled low-carbon sheet and strip to IS 513.
- Hot-rolled (HR) sheet and plate: finished hot, so the surface carries blue-grey mill scale, edges may be slightly rounded and thickness tolerance is wider. It is cheaper and is used for structural members, chassis frames, tanks and anything that will be welded and painted.
- Cold-rolled (CR) sheet: made by pickling HR coil to remove scale, cold rolling it thinner, then annealing it (to restore formability) and giving it a light skin pass. It has a smooth, bright surface, close thickness tolerance and good drawability, and is used for car body panels, appliance cabinets, furniture and anything that needs a good painted or plated finish.
For how both are cut, bent and joined, see sheet metal fabrication.
Advantages and limitations
Hot working
Advantages:
- Much lower forces, so large shapes can be made with large reductions per pass.
- Refines grain, closes porosity and welds shut internal voids in cast ingots.
- Metal stays ductile; no annealing is needed between stages.
- Grain flow can be directed to follow the part, improving fatigue and impact strength.
Limitations:
- Oxide scale and a rough surface; some decarburisation of steel.
- Poor dimensional accuracy, as the part shrinks on cooling.
- Heating costs, and tooling and handling at high temperature.
- Properties can vary through the section if finishing temperature is not controlled; finishing too hot leaves coarse grain.
Cold working
Advantages:
- Higher strength and hardness from strain hardening, without heat treatment.
- Bright, smooth surface and close tolerances, often needing no machining.
- No heating and no scale; good for thin sheet, wire and small parts in high volume.
Limitations:
- High forces and power; heavier presses and tooling.
- Loss of ductility; the metal may crack and need intermediate annealing.
- Residual stresses that can cause distortion or stress-corrosion cracking.
- Not practical for hard or thick sections, or for metals with limited ductility, where cold forming increases the risk of brittleness and cracking.
Cold-worked parts are often annealed or stress relieved afterwards, and hot-worked parts are often normalised; both are covered on the heat treatment of steel page. Process data for specific alloys is published by ASM International.
FAQs
What is the main difference between hot working and cold working?
Hot working is done above the metal’s recrystallisation temperature, so it does not strain harden; cold working is done below it, so the metal gets stronger and harder but less ductile. The line depends on the metal, not on a fixed temperature.
Is working steel at 400 °C hot or cold working?
For ordinary steel it is below the recrystallisation temperature (roughly 450-630 °C by the 0.4-0.5 Tm rule), so strictly it is cold or warm working, even though the steel is hot to touch.
How do you calculate percent cold work?
Percent cold work = (A0 – Af) / A0 × 100, using cross-sectional areas. Drawing a 5 mm wire to 4 mm gives 36%; rolling a 3 mm sheet to 2 mm gives 33.3%.
Why is cold-rolled steel stronger than hot-rolled steel?
Cold rolling strain hardens the steel, raising its yield strength and hardness. If the cold-rolled sheet is then fully annealed for deep drawing, much of that extra strength is removed; what remains is the better surface and tighter tolerance.
Why does cold working reduce ductility?
Plastic deformation multiplies dislocations, which tangle and block each other. The metal then has less capacity to deform further before cracking. Annealing recrystallises the grains and restores the ductility.