 EngineeringHulk
- Home
- Blog
- Manufacturing Engineering
- Welding Aluminium: Techniques, Challenges, Filler Choice and Applications
Welding Aluminium: Techniques, Challenges, Filler Choice and Applications
On this page
Welding aluminium is harder than welding steel because its surface oxide melts at about 2050 °C while the metal underneath melts at about 660 °C, and because aluminium conducts heat away several times faster than steel. The standard answer is AC TIG for thin and precise work and MIG with pure argon and a spool gun or push-pull feeder for faster work, on a surface that has been degreased and stainless-brushed just before welding. The filler is usually 4043 or 5356, chosen by base alloy.
For where TIG and MIG sit among the other processes, see our types of welding hub. This page covers only what changes when the metal is aluminium.
Why is aluminium hard to weld?
1. The oxide layer
Aluminium forms a thin, hard film of aluminium oxide (Al2O3) the moment it meets air. The oxide melts at about 2050 °C, roughly three times the melting point of the metal. If it is not removed, the metal below melts first while the oxide skin stays solid on top, so the filler balls up instead of flowing in, and oxide fragments get trapped as inclusions. The film is also porous and holds moisture and grease, which feed porosity.
2. High thermal conductivity
Aluminium carries heat away from the arc several times faster than steel. The start of a weld feels cold and lacks fusion; a few centimetres later the whole part has heated up and the same current now burns through. Welders deal with this by using more current at the start, moving faster as the part warms, and preheating thick sections.
3. No colour warning
Steel glows red, then orange, before it melts. Aluminium stays silvery until it suddenly slumps, so beginners burn through thin sheet without warning.
4. Hydrogen porosity
Molten aluminium dissolves far more hydrogen than solid aluminium. As the pool freezes, the hydrogen comes out as gas bubbles that stay trapped as porosity. The hydrogen comes from moisture, grease, hydrated oxide and damp filler wire, which is why cleanliness matters more than on steel.
5. Hot cracking
Aluminium shrinks a lot on solidifying, and some alloys (notably 6xxx and 2xxx) are prone to solidification cracking in the weld and in the crater at the end of the bead. The right filler and filling the crater before stopping are the main cures.
6. HAZ softening
Heat-treatable alloys such as 6061-T6 get their strength from fine precipitates produced by heat treatment. The welding heat dissolves and coarsens them, so the heat-affected zone ends up much weaker than the parent metal. The worked example below puts a number on it. Work-hardened alloys (such as 5083-H321) lose their work hardening in the HAZ in the same way.
AC TIG welding of aluminium
TIG is the go-to process for thin aluminium, tubes, and any weld that must look good. It is run on alternating current because each half of the AC cycle does a different job:
| Half-cycle | Electrode polarity | What it does |
|---|---|---|
| Cleaning half | Electrode positive (EP) | Electrons leave the work and blast the oxide film off the surface (cathodic cleaning). Heats the tungsten more. |
| Penetration half | Electrode negative (EN) | Most heat goes into the work, giving penetration. Keeps the tungsten cool. |
AC balance on an inverter machine sets how much of each cycle is EN. More EN gives deeper penetration, a narrower bead and a sharper tungsten; more EP gives a wider cleaned (etched) zone either side of the bead but a hotter, balling tungsten. Starting points of roughly 65-75% EN are typical; increase EP only if the oxide is not being cleaned. Many inverters also let you raise the AC frequency to tighten the arc.
Other TIG points: use pure argon (argon-helium mixes for thick sections), a clean tungsten (not pure tungsten on modern inverters; lanthanated or zirconiated types are common), and push the rod into the leading edge of the pool rather than dripping it from above. More on the process: TIG welding.
MIG welding of aluminium
MIG is much faster than TIG and is used for thicker sections, boat hulls, trailers and production work. Aluminium wire is soft, so it kinks and “bird-nests” if pushed through a long steel-wire liner. The fixes are:
- Spool gun: a small spool of wire sits on the gun itself, so the wire only travels a few centimetres. Cheap and common on workshop machines.
- Push-pull feeder: a motor in the gun pulls the wire while the machine pushes it, so long torch cables can be used in production.
- Use a Teflon or nylon liner, U-groove drive rolls, light roll pressure and a contact tip one size oversize (the wire expands with heat).
Use 100% argon (not the argon-CO2 mix used for steel), a spray or pulsed-spray transfer, and a push (forehand) gun angle so the gas shield reaches the pool ahead of the arc. MIG runs on DCEP, which gives the same oxide-cleaning action as the EP half of AC TIG. See also MIG welding.
Choosing the filler: 4043 or 5356?
4043 is an aluminium-silicon filler; 5356 is aluminium-magnesium. Hobart’s filler-selection guidelines give the main rules:
| Situation | Use | Why |
|---|---|---|
| 6xxx base metal (6061, 6063), or 5xxx with up to 2.5% Mg (such as 5052) | Either 4043 or 5356 | Both work; choose on the other rows |
| 5xxx with more than 2.5% Mg (5083, 5086, 5456) | 5356, never 4043 | Si from 4043 plus high Mg forms brittle Mg2Si, reducing ductility and raising crack sensitivity |
| Long service above about 65 °C (150 °F) | 4043 (or 5554), not 5356 | 5356 welds can become crack sensitive at sustained elevated temperature |
| Part will be anodised and must match in colour | 5356 | 4043 welds turn dark grey after anodising |
| Fillet welds needing high shear strength | 5356 | Higher shear strength per pass |
| Crater and shrinkage cracking is a problem | 4043 | Silicon makes the pool more fluid and less crack sensitive |
| MIG wire feeding | 5356 is easier | Stiffer wire feeds better |
In short: 4043 for 6061 when cracking resistance, a bright bead or heat service matters; 5356 for marine 5083/5086 plate, anodised parts and strong fillets.
Preparing aluminium for welding
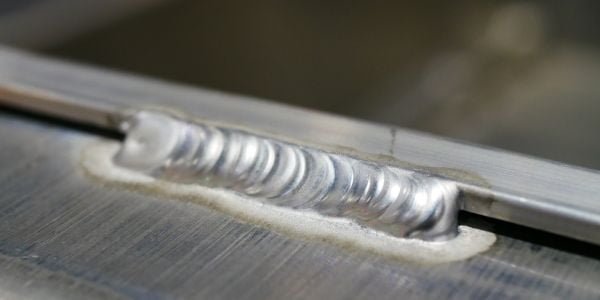
- Degrease first: wipe with acetone or a solvent on a clean, lint-free cloth. Brushing a greasy surface only spreads the grease.
- Remove the oxide: use a stainless-steel wire brush kept only for aluminium. A brush used on carbon steel embeds iron particles; do not use grinding discs loaded with other metals either.
- Weld soon: the oxide starts to regrow at once. Brush and weld within a few hours, not the next day.
- Keep filler dry and clean: store wire and rods sealed, and wipe TIG rods before use.
- Preheat only thick sections: preheating helps fusion on thick plate and heavy castings. For heat-treatable alloys keep it modest (a typical upper limit is around 120 °C) and check it with a temperature crayon, because extra heat widens the soft HAZ.
- Fit-up and backing: tack closely, use a backing bar on thin sheet, and add run-off tabs or fill the crater at the end to stop crater cracks.
Worked example: HAZ strength loss in 6061-T6
ESAB notes that 6061-T6 has a typical tensile strength of about 45 ksi before welding, that the AWS D1.2 structural aluminium code sets a minimum as-welded tensile strength of 24 ksi, and that fully annealed 6061 is about 18 ksi. Convert with 1 ksi = 6.895 MPa:
- Unwelded, typical: 45 × 6.895 = 310 MPa
- As-welded, code minimum: 24 × 6.895 = 165 MPa
- Fully annealed, typical: 18 × 6.895 = 124 MPa
Take a 6 mm × 100 mm flat bar of 6061-T6 with a full-penetration butt weld across it. Area A = 6 × 100 = 600 mm2.
- Breaking load of plain bar ≈ 310.3 × 600 = 186,200 N = 186 kN
- Design breaking load across the weld (code minimum) = 165.5 × 600 = 99,300 N = 99 kN
- Strength retained = 24 / 45 = 0.53, so about 47% of the strength is lost at the weld.
The lesson for design: a welded 6061-T6 joint is not as strong as the bar. Either size the section for as-welded properties, place welds in low-stress areas, or re-solution treat and age the whole part after welding (expensive and it distorts). The softening is caused by heat, not by the filler, so extra heat input makes it worse.
Other processes for aluminium
- Friction stir welding: a solid-state process, so no melting, no porosity and less HAZ softening. Widely used for aluminium ship decks, rail coach panels and rocket tanks.
- Laser welding: low heat input and high speed; used for car bodies and battery enclosures, though aluminium’s high reflectivity makes it harder than steel.
- Resistance spot welding: possible but needs much higher current than steel and frequent electrode dressing.
- Stick (SMAW) electrodes for aluminium exist but give poor, spattery welds and are used only for emergency repairs.
Research on the inert gas shielding of aluminium arcs and the procedure codes of the American Welding Society (AWS) are good next references.
Applications of aluminium welding
- Transport: rail coaches and metro car bodies, truck bodies and tippers, trailers, two-wheeler frames.
- Marine: boat hulls and superstructures in 5083/5086 plate, welded with 5356.
- Aerospace and space: fuel tanks and structures (often by friction stir or TIG).
- Process plant: tanks and pressure vessels, cryogenic equipment, heat exchangers.
- Building and fabrication: window and facade frames, ladders, railings, bicycle frames.
FAQs
Why is aluminium difficult to weld?
Its oxide layer melts at about 2050 °C while the metal melts at about 660 °C, it conducts heat away very quickly, it gives no colour warning before melting, it absorbs hydrogen that causes porosity, and heat-treatable grades lose strength in the heat-affected zone.
Which welding is best for aluminium?
AC TIG is best for thin sheet, tubes and high-quality visible welds. MIG with 100% argon and a spool gun or push-pull feeder is best for thicker sections and faster production. Friction stir welding is used in industry for long, high-quality seams.
Should I use 4043 or 5356 filler?
Use 5356 for 5xxx alloys with more than 2.5% magnesium (such as 5083), for anodised parts and for high-strength fillets. Use 4043 for crack-prone 6xxx joints and for parts that will run above about 65 °C. For 6061 either works.
Why is AC used for TIG welding aluminium?
The electrode-positive half of each cycle breaks up the oxide film (cleaning action), and the electrode-negative half puts heat into the work for penetration. AC balance sets the split between the two.
Can you weld aluminium with a normal MIG welder?
Yes, if it can be fitted with a spool gun or has a push-pull torch, and you change to pure argon, a Teflon liner, U-groove drive rolls and aluminium contact tips. A standard steel setup usually tangles the soft wire.
Related Topics on EngineeringHulk
Keep reading
Cold Welding: How It Works, Process, Metals and Applications
How does cold welding work? Pressure breaks the oxide film so clean metal atoms bond at room temperature. Process, metals, space and wiring uses, limits.
Flux Core Welding (FCAW): Types, Technique, Wire Codes and Applications
Flux core welding explained: self-shielded vs gas-shielded FCAW, polarity, reading E71T-1C and E71T-11, technique, slag, uses and a deposition example.
Stick Welding (SMAW): Equipment, Electrodes, Techniques and Defects
Stick welding (SMAW) joins steel with a flux-coated consumable electrode. Equipment, polarity, AWS and IS 814 electrode codes, amps and defects.

Brazing Process: Joint Design, Filler Metals, Steps and Applications
What is brazing? Filler melting above 450 C is drawn into a tight joint by capillary action. Joint clearance, flux, heating methods, fillers and uses.

TIG Welding (GTAW): Process, Equipment, Polarity, Technique and Applications
TIG welding explained: how GTAW works, torch and tungsten types, DCEN and AC polarity, shielding gases, current settings and the usual defects.
Types of Welding: Processes, Advantages, Disadvantages and Applications
Types of welding explained: arc (SMAW, MIG, TIG, SAW, FCAW), gas, resistance, beam and solid-state welding, with a comparison table and heat input example.