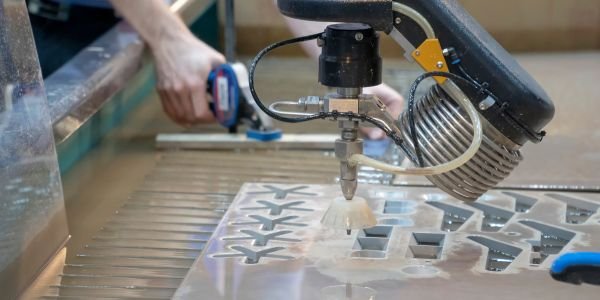
Abrasive jet machining (AJM) removes material by blasting a fine stream of dry abrasive particles, typically 10 to 50 microns in size and carried in compressed air or gas, at the workpiece at about 100 to 300 m/s. Each particle that strikes the surface chips out a microscopic fragment, so AJM works best on hard, brittle and heat-sensitive materials such as glass, ceramics, quartz and silicon. It is also called abrasive air jet machining or micro-abrasive blasting.
AJM is a close relative of sandblasting, but it uses much finer abrasive, a small nozzle (0.2 to 0.8 mm bore) and tightly controlled pressure, flow and distance. That control is what turns blasting into a machining process.

How does abrasive jet machining work?
Compressed gas at a few bar is mixed with abrasive powder and forced through a nozzle. The nozzle converts the gas pressure into velocity, and the gas drags the particles up to jet speed. When a particle hits a brittle surface, its kinetic energy creates a small indentation with cracks around and below it. The cracks meet and a tiny chip breaks away. On ductile materials the particles tend to plough or cut small grooves instead, which is slower and can leave grit embedded in the surface.
There is no contact between nozzle and work, so the cutting force is tiny and the process runs cold. The spent abrasive and debris are sucked away by a dust collector.
Abrasive jet machining set-up and main parts

| Part | Function | Typical details |
|---|---|---|
| Compressor or gas cylinder | Supplies the carrier gas | Air, nitrogen or CO2; oxygen is not used |
| Pressure regulator | Sets the working pressure | About 2 to 10 bar; around 5 bar is common |
| Dryer and filters | Remove moisture, oil and dirt so the powder does not clump or clog the nozzle | Dry, clean air is essential |
| Mixing chamber with vibrator | Abrasive falls from a hopper through a sieve that is vibrated electromagnetically; the vibration amplitude sets how much powder enters the gas | Sieve vibrated at about 50 to 60 Hz |
| Nozzle | Accelerates and directs the abrasive jet | Tungsten carbide (life about 12 to 30 hours) or synthetic sapphire (about 300 hours); bore 0.2 to 0.8 mm |
| Machining chamber and dust collector | Contains the jet and extracts dust | Closed cabinet with vacuum extraction |
| Work table | Holds and moves the work under the jet, or the nozzle is moved over it | Manual, pantograph or CNC control |
Abrasive is not reused. Once the sharp edges are worn it cuts poorly, and the fines can clog the nozzle.
AJM process parameters and their effects
| Parameter | Typical range | Effect |
|---|---|---|
| Abrasive type | Al2O3, SiC, glass beads, crushed glass, sodium bicarbonate | Al2O3 is the general-purpose choice; SiC is harder and faster on very hard work; glass beads give a matte polish; sodium bicarbonate is used for gentle cleaning |
| Grain size | 10 to 50 microns | Coarser grains remove more per impact; finer grains give better finish and sharper detail |
| Abrasive mass flow rate | 2 to 20 g/min | About 2 to 4 g/min for fine work and 10 to 20 g/min for cutting |
| Mixing ratio | Mass of abrasive / mass of gas | MRR rises to an optimum, then falls (see below) |
| Gas pressure | 2 to 10 bar | Higher pressure means higher jet velocity and higher MRR, but faster nozzle wear |
| Jet velocity | 100 to 300 m/s | Impact energy rises with the square of velocity |
| Nozzle tip distance (stand-off) | About 0.5 to 15 mm; a few mm is common | Sets MRR, spot size and taper (see below) |
| Impingement angle | 60 to 90 degrees | Near 90 degrees for drilling brittle work; lower angles for cleaning and deburring |
MRR vs nozzle tip distance
MRR first rises as the nozzle tip distance (NTD) increases, because the particles keep accelerating for a short distance after leaving the nozzle. It reaches a peak and then falls, because the jet spreads out and slows down. At the same time the machined spot gets wider and the walls become more tapered. A short NTD gives a small, sharp, deep cut but wears the nozzle faster from rebounding grit; a long NTD suits cleaning and frosting over wider areas.

MRR vs abrasive flow rate and mixing ratio
If the gas flow is held constant, adding more abrasive at first raises MRR because more particles hit the work. Beyond a point, the same gas has to accelerate more powder, each particle leaves slower, and particles collide with one another, so MRR falls. That is why there is an optimum mixing ratio. If instead the mixing ratio is held constant (gas flow increased along with abrasive flow), MRR keeps rising with abrasive flow.
Worked example: estimating MRR
The NPTEL (IIT Kharagpur) model assumes each spherical particle spends all its kinetic energy making a hemispherical crater in a brittle surface. It gives, to a close approximation (the exact constant is 4/63/4, about 1.04):
MRR ≈ ma v3/2 / (ρg1/4 H3/4)
where ma = abrasive mass flow rate, v = particle velocity, ρg = abrasive density and H = flow strength (hardness) of the work.
Problem: a brittle material with H = 4 GPa is machined with abrasive at 2 g/min, velocity 200 m/s and density 3 g/cm3. Estimate MRR.
- ma = 2 g/min = 0.002 / 60 = 3.33 × 10⁻⁵ kg/s
- v3/2 = 2001.5 = 2828
- ρg1/4 = 30000.25 = 7.40 (kg/m3)
- H3/4 = (4 × 10⁹)0.75 = 1.59 × 10⁷ (Pa)
MRR = (3.33 × 10-5 × 2828) / (7.40 × 1.59 × 107) = 8.0 × 10⁻¹⁰ m3/s = 0.80 mm3/s ≈ 48 mm3/min.
Treat this as an upper estimate. Real jets lose energy to rebound, particle break-up and heating, and the same NPTEL notes quote around 15 mm3/min as a practical MRR for glass. The formula is most useful for trends: MRR is directly proportional to abrasive flow and rises with velocity to the power 1.5.
Advantages of abrasive jet machining
- Cold process: no heat-affected zone, so heat-sensitive materials are safe.
- Very low force and no tool contact, so thin, fragile parts do not crack or chatter.
- Cuts hard, brittle materials regardless of electrical conductivity.
- Can reach awkward spots and cut intricate shapes and fine slots.
- Shallow surface damage (a few microns).
- Low capital cost and simple equipment.
Limitations of AJM
- Low MRR. Suitable for small, fine jobs, not bulk removal. Practical cutting is limited to thin sections, of the order of 1.5 mm in steel and about 6 mm in glass.
- Taper. The jet flares as it leaves the nozzle, so holes and slots are wider at the top.
- Stray cutting. The spreading jet erodes areas next to the target unless they are masked with rubber, metal or photoresist.
- Dust and health risk. A closed cabinet and dust extraction are mandatory.
- Nozzle wear. A worn nozzle widens the jet and hurts accuracy.
- Embedded grit. On soft materials such as elastomers and soft plastics, particles lodge in the surface.
- Abrasive cannot be reused.
Applications of abrasive jet technology
- Deburring: removing fine burrs from small holes, hypodermic needles, milled slots and plastic parts.
- Frosting and engraving glass: matte finishes, logos, and registration numbers etched on car window glass.
- Cleaning: removing oxides from metals, metallic smears from ceramics and coatings from electronic parts.
- Cutting thin brittle sections: slicing and slotting glass, quartz, sapphire, mica, silicon and germanium.
- Electronics: drilling glass wafers, trimming resistors and cutting semiconductor material.
- Deflashing small castings and moulded parts.
Abrasive jet micro machining
Abrasive jet micro machining uses very fine powder, low pressure and a patterned mask to cut channels, holes and cavities of well under a millimetre in glass and silicon. It is used for microfluidic chips, sensors and MEMS devices, where the mask defines the shape and the jet does the erosion, much like photochemical etching but mechanical and fast on glass.
Abrasive jet machining vs abrasive water jet machining
The names are similar but the machines are not. AJM uses dry abrasive in air or gas at a few bar and suits fine work on thin brittle parts. Abrasive water jet machining (AWJM) uses water pressurised to about 2500 to 4000 bar by an intensifier, draws garnet abrasive into the water jet in a mixing tube, and can cut steel plate tens of millimetres thick. For more on the water-based process see our guide to waterjet machines.
| Point | AJM | AWJM |
|---|---|---|
| Carrier | Air, N2 or CO2 | Water |
| Pressure | About 2 to 10 bar | About 2500 to 4000 bar |
| Typical abrasive | Al2O3, SiC, 10 to 50 microns | Garnet, olivine |
| Work | Thin, brittle, fine features | Metals, stone, composites, thick plates |
| Main use | Deburring, frosting, cleaning, micro-cutting | Profile cutting of plate |
AJM is one of the mechanical non-traditional processes, alongside ultrasonic machining, which also uses abrasive impact but drives the grains with a vibrating tool instead of a gas jet. For the wider family of processes see material removal techniques in manufacturing. Parameter ranges here follow the NPTEL (IIT Kharagpur) lesson on AJM; the topic is part of the AICTE model curriculum for non-traditional machining.
FAQs
What is the principle of abrasive jet machining?
Fine abrasive particles carried in a high-velocity gas jet strike the workpiece. Their kinetic energy causes small cracks and brittle fracture, chipping away tiny fragments of material. Removal is by erosion, with no tool contact and almost no heat.
Which abrasives are used in AJM?
Aluminium oxide and silicon carbide are the most common, in sizes of about 10 to 50 microns. Glass beads are used for polishing and matte finishing, and sodium bicarbonate for light cleaning.
Why are AJM nozzles made of tungsten carbide or sapphire?
The abrasive stream erodes the nozzle bore, so the nozzle must be extremely wear-resistant. Tungsten carbide nozzles last roughly 12 to 30 hours and sapphire nozzles about 300 hours before the bore wears enough to spoil accuracy.
How does nozzle tip distance affect MRR in AJM?
MRR increases with nozzle tip distance up to a peak and then decreases as the jet spreads and slows. Increasing the distance also widens the cut and increases taper.
Can abrasive jet machining cut metals?
Only thin sections, of the order of 1.5 mm in steel, and slowly. Ductile metals deform rather than chip, and grit can become embedded. AJM is mainly used on metals for deburring and cleaning, not cutting.