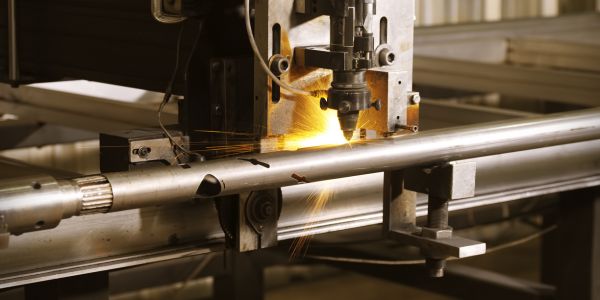
Laser etching is a laser marking process that melts a very thin surface layer of a material so that it re-solidifies with a raised, roughened or differently reflective texture, giving a permanent, high-contrast mark with almost no material removed. A laser etching machine does this with a pulsed laser (usually fibre, sometimes UV or CO2) and a pair of fast scanning mirrors that write text, logos, barcodes and serial numbers onto metal and plastic parts in seconds.
Laser etching vs engraving vs marking: what is the difference?
All four processes can run on the same machine; they differ in what happens to the surface:
- Etching: the top layer melts and re-solidifies. The mark is very shallow and gets its contrast from the changed texture, which scatters light differently from the untouched surface.
- Engraving: the laser vaporises material to leave a recess you can feel and measure. It takes more energy per millimetre and more passes.
- Annealing (colour) marking: the surface of a metal such as stainless steel or titanium is heated below melting so that a thin oxide layer grows. The oxide shows as black or as colours, and the surface stays smooth, which is why it is used on medical instruments that must not trap dirt.
- Ablation: the laser removes a coating (paint, anodising dye, a printed layer) to expose the material underneath, for example white text on a black anodised aluminium panel.
For a side-by-side table of depth and examples, see the comparison on our laser engraver page. The short version: etching sits between marking and engraving. Exact depth depends on the material and settings, so treat any single depth figure with care.
How does a laser etching machine work?
Most industrial etching machines are “galvo” markers. The work sits still and the beam moves:
- The source fires short pulses. A pulsed fibre laser (about 1 µm wavelength) is the usual choice for metals. Each pulse lasts nanoseconds, so it heats a tiny spot very hard and very briefly. How the laser itself makes light is covered on our laser basics page.
- A beam expander widens the beam so that it can be focused to a smaller spot.
- The galvanometer scanner has two small mirrors mounted on fast motors: one deflects the beam in X, the other in Y. Because the mirrors are tiny and light, the spot can be moved across the field at hundreds to thousands of millimetres per second.
- The f-theta lens focuses the beam and keeps the focal spot on a flat plane across the whole marking field. An ordinary lens would focus on a curved surface, blurring the corners.
- The controller converts the design (text, vector logo, barcode, a serial number that increments on each part) into mirror angles and laser on/off commands, filling areas with closely spaced hatch lines.
The pulse melts a spot perhaps a few tens of micrometres across (typical order of magnitude). As overlapping pulses march along each hatch line, the melted track freezes with a slightly raised, rippled surface. That texture is the mark.
Parts of a laser etching machine
| Part | Function |
|---|---|
| Laser source | Pulsed fibre (metals, many plastics), UV (heat-sensitive plastics, glass) or CO2 (wood, paper, glass, organic materials). Power for marking is usually tens of watts. |
| Beam expander | Enlarges the beam diameter for a smaller focused spot |
| Galvo scanner head | Two motor-driven mirrors that steer the beam in X and Y |
| F-theta (flat-field) lens | Focuses the beam onto a flat marking field; a longer focal length gives a bigger field but a larger spot |
| Z-axis column | Raises or lowers the head so the part surface sits at the focal distance |
| Red pointer / preview laser | A visible guide beam that traces the mark outline so the operator can position the part |
| Controller and software | Imports designs, generates hatch fills, serial numbers, date codes and 2D codes, and links to a PLC on production lines |
| Work table or fixture, rotary axis | Holds parts in a repeatable position; a rotary attachment marks around cylinders |
| Enclosure and fume extractor | Blocks stray radiation and removes the fume released from the surface |
Materials and typical uses
- Steel and stainless steel: part numbers, heat numbers, logos on tools. Stainless can take black or coloured annealing marks as well as etched marks.
- Anodised aluminium: nameplates, front panels, electronics housings. The laser removes or bleaches the dyed layer to give white or grey text.
- Traceability codes: serial numbers, barcodes and Data Matrix codes on automotive and aerospace parts, and UDI (unique device identification) codes on medical devices, which must survive cleaning and sterilisation.
- Plastics: keycaps, switch panels, cable markers. Many plastics foam or change colour rather than etch; UV sources give the cleanest marks on heat-sensitive grades.
- Glass, wood and leather: handled by CO2 etching machines, which frost glass and darken wood.
- Jewellery and consumer goods: personalisation of rings, pens, phone cases and tumblers.
Key parameters
| Parameter | What it controls |
|---|---|
| Average power (W) | Total heat into the surface; more power gives a stronger mark |
| Marking speed (mm/s) | How fast the spot moves; higher speed means less energy per mm and a lighter mark |
| Pulse frequency (kHz) | Pulses per second. Pulse energy = power / frequency, so a higher frequency gives more, weaker pulses |
| Pulse spacing | Speed / frequency; it must be smaller than the spot size or the mark breaks into separate dots |
| Hatch spacing (mm) | Gap between fill lines; smaller spacing gives a denser, more even mark but takes longer |
| Focus distance | At focus the spot is smallest and sharpest; slightly defocused gives a softer, wider mark |
| Pulse duration (MOPA fibre lasers) | Short pulses for crisp marks on plastics and anodising; longer pulses for more heat, used for colour and black marks on metals |
Worked example: how long does a mark take?
Job: fill-etch a serial-number block 40 mm long and 10 mm high on a steel part. Assumed settings (for illustration): 20 W pulsed fibre laser, 20 kHz, marking speed 1000 mm/s, hatch spacing 0.05 mm, fill lines running along the 40 mm length.
- Number of hatch lines = 10 / 0.05 = 200 lines
- Total hatch length = 200 × 40 mm = 8000 mm
- Marking time for the full block = 8000 / 1000 = 8 s
- If the characters cover only about 40% of the block (an assumption; it depends on the font), beam-on time falls to about 0.4 × 8 = 3.2 s, plus short jump moves between characters
Two more numbers from the same settings:
- Pulse energy = 20 W / 20,000 pulses per second = 0.001 J (1 mJ)
- Pulse spacing = 1000 mm/s / 20,000 per s = 0.05 mm along each line
Now double the speed to 2000 mm/s. The time halves to 4 s for the full block, but the pulse spacing doubles to 0.1 mm. If the focused spot is smaller than that, the pulses no longer overlap and the line turns into a row of dots. To keep the same spacing at the higher speed you would also have to double the frequency to 40 kHz, which halves the pulse energy. Halving the hatch spacing to 0.025 mm instead doubles the line count and the time goes up to 16 s. Every setting trades time against mark quality, which is why shops run a test matrix on a scrap part before production.
Advantages of laser etching
- Permanent marks that resist wear, heat and most chemicals, unlike ink, labels or stickers
- Non-contact: no tool wear, no clamping forces, suits delicate and finished parts
- Fast: short codes are marked in seconds, making in-line marking on production lines practical
- Variable data such as serial numbers, dates and 2D codes change automatically from part to part
- No consumables such as ink, solvents or chemical etchants (unlike chemical etching)
- Fine detail, down to small readable text and dense codes
Limitations
- Shallow: the mark can be removed by grinding, blasting or heavy wear, where deep engraving or stamping would survive
- The melted surface layer can reduce corrosion resistance on stainless steel if the settings are too aggressive
- Each source suits certain materials: fibre lasers do not mark clear glass well; CO2 does not mark bare metal
- Small marking field per position; large parts need repositioning or a moving table
- Machine cost is high compared with ink-jet coding or stamping
Safety
Marking sources of tens of watts are Class 4 lasers. Buy or build a fully enclosed, interlocked station (which makes it a Class 1 product in normal use), or use wavelength-matched safety glasses with an adequate optical density. The 1 µm light from a fibre laser is invisible, so you cannot see a stray reflection. Fume extraction is needed because melted metal and plastics release fine particles and gases. Never mark PVC.
For cutting right through the material instead of marking it, see our laser cutting machine guide, and for the source behind most etching machines, the fibre laser. Laser beam machining is covered in the NPTEL manufacturing processes courses.
FAQs
What is a laser etching machine?
A laser etching machine is a marking system that uses a pulsed laser and scanning mirrors to melt a very thin surface layer of a part, creating a permanent, high-contrast mark such as text, a logo or a barcode.
What is the difference between laser etching and laser engraving?
Etching melts only the surface so it changes texture and contrast, with very little depth. Engraving vaporises material to leave a recess you can feel. Etching is faster; engraving survives more wear.
Which laser is used for laser etching of metal?
A pulsed fibre laser at about 1 micrometre wavelength is the usual choice for metals, because metals absorb this wavelength well. MOPA fibre lasers, with adjustable pulse duration, are used for black and colour marks on stainless steel and anodised aluminium.
Is laser etching permanent?
Yes. The mark is part of the material surface, so it does not fade, smudge or peel. It can only be removed by taking off the surface layer, for example by grinding or polishing.
Can you laser etch plastic?
Yes, many plastics can be marked. Depending on the plastic and source, the mark forms by foaming, colour change or light etching. UV lasers give the finest, lowest-heat marks on heat-sensitive plastics. PVC must not be marked because it releases hydrogen chloride gas.