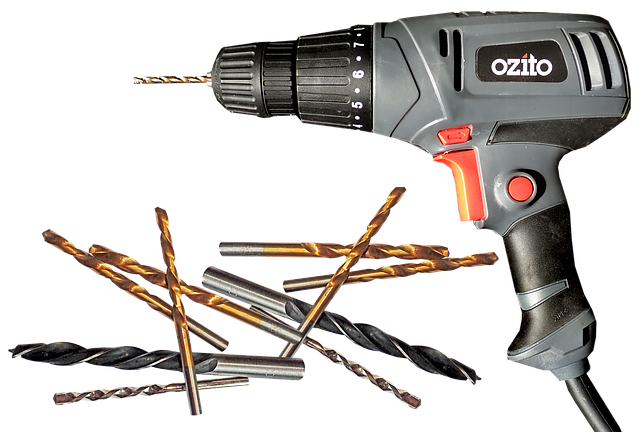
A drill bit is the rotary cutting tool that actually makes the hole: it is held in the drill chuck or spindle taper, rotates about its own axis, and shears material away with the cutting lips at its point while the flutes carry the chips back out. The general-purpose type is the two-flute twist drill, ground to a 118 degree point angle with a helix angle around 25 to 30 degrees, and made in metric sizes from 0.5 mm upward. Change the material, and you change the bit: masonry needs a carbide tip and hammer action, timber needs a lead screw or a spur, thin sheet needs a step bit.

Parts of a drill bit
Every term in a workshop drawing of a twist drill comes from ISO 5419, which defines twist drill terms, definitions and types. These are the parts you need to be able to name and point at.
| Part | Where it is | What it does |
|---|---|---|
| Shank | The plain end held by the machine | Parallel (straight) shank up to about 13 mm for chuck holding, or a Morse taper shank above that which drives directly into the spindle nose. Some parallel shanks are reduced so a 16 mm drill still fits a 13 mm chuck. |
| Tang | Flattened end of a taper shank | Sits in a slot in the spindle. It stops the drill slipping under heavy torque and gives the drift key something to push against when you knock the tool out. |
| Body | Between shank and point | The fluted working length. It is ground with a slight back taper, typically 0.02 to 0.08 mm per 100 mm, so the drill does not bind in a deep hole. |
| Flutes | The two helical grooves | Form the cutting lips, evacuate chips and let coolant reach the point. Flute shape, not just depth, decides whether chips curl and clear or pack and jam. |
| Land and margin | Raised strip between the flutes | The margin is the narrow full-diameter strip along the land edge. Only the margin touches the hole wall, which keeps the drill guided while cutting friction low. |
| Web | Central core between the flutes | The backbone of the drill. It thickens towards the shank for strength, which is why a much-resharpened drill gets a wider chisel edge and cuts badly until the web is thinned. |
| Point | The conical cutting end | Carries the two lips, the chisel edge and the clearance faces. The whole performance of the drill lives here. |
| Lips (cutting edges) | The two main edges at the point | Do the cutting. They must be equal in length and equally angled about the axis; if not, one lip does all the work and the hole comes out oversize. |
| Chisel edge | Where the two clearance faces meet at the centre | Does not cut so much as extrude. It can account for a large share of the thrust force, and it is the reason an unpunched drill wanders off the mark. |
| Lip relief (clearance) | Behind each cutting lip | Typically 8 to 12 degrees at the outer corner, rising toward the centre. No relief means the heel rubs and the drill will not penetrate. |

Point angle and helix angle: the numbers that matter
Two ground angles separate a drill that cuts cleanly from one that squeals and burns.
Point angle
- 118 degrees is the general-purpose standard, ground as a conventional chisel-edge point. It is a little more aggressive, it penetrates mild steel, cast iron, brass and timber happily, and it is what you get in an ordinary jobber drill set.
- 135 degrees is the flatter point, almost always supplied as a split point. The flatter geometry is stronger and holds its edge longer in hard material, and the split grind cuts the chisel edge down to a short self-centring point, so the drill starts on its own without a centre punch and without walking on a curved or slippery surface. This is the choice for stainless steel, alloy steel and tool steel.
- Around 90 degrees is used for plastics and some soft non-ferrous work, where a sharp point would grab and pull the drill through.
- 140 degrees and flatter appears on carbide drills for hardened material, where edge strength beats everything else.
Helix angle
The helix angle is the angle between the leading edge of the land and the drill axis. It controls chip flow and rake. Drills are classified by it in DIN 1836 as type N, H and W.
| Type | Helix angle | Suits |
|---|---|---|
| Type N, normal helix | About 19 to 40 degrees, commonly 25 to 30 | The default. Structural and mild steel, cast iron, most non-ferrous metals. This is what a standard jobber drill is. |
| Type H, slow helix | About 10 to 19 degrees | Hard, brittle, short-chipping material: brass, bronze, hard plastics, acrylic and laminates. The low helix reduces rake so the drill cannot snatch and pull itself into the work. |
| Type W, quick helix | About 35 to 45 degrees | Soft, long-chipping, gummy material: aluminium, copper, soft plastics. The steep flute keeps stringy chips moving instead of welding into the flute. |
A practical consequence students often miss: drilling brass with a standard type N drill makes the bit grab and dig in as it breaks through. The shop fix is to stone a small flat on the cutting lips to kill the rake, which turns a type N drill into something closer to a type H.
Types of drill bits
Twist drill
Two helical flutes, 118 degree point, parallel or taper shank. It does most hole making in metalworking, wood and plastic between 0.5 mm and about 50 mm. Jobber length is the general-purpose length; stub (screw machine) length is shorter and stiffer for accuracy; long series reaches deeper.
Centre drill and spot drill
A short, very stiff bit used only to start a hole accurately. The centre drill has a small pilot with a 60 degree countersink and is meant for producing lathe centres; the spot drill is a single short flute ground to 120 or 142 degrees purely to make a starting dimple for the following drill. Use one and a wandering drill problem disappears.
Step drill
A conical bit with stepped diameters, each step a separate size. Drills and deburrs in one plunge and is made for sheet metal up to a few millimetres thick, where a twist drill would grab and tear a triangular hole. A single 4 to 20 mm step bit replaces a whole set for panel and electrical work.

Countersink
Cuts a cone at the mouth of an existing hole so a flat-head screw sits flush. Usually 90 degrees for metric screws, 82 degrees for imperial. Also the quickest way to deburr a hole edge.
Counterbore
Cuts a larger flat-bottomed recess at the hole mouth, with a pilot that runs in the existing hole to keep it concentric. Used so a socket head cap screw or a washer sits below the surface.
Spade or flat bit
A flat blade with a centre spur on a hex shank, for fast rough holes in timber from about 6 to 38 mm. Cheap, easy to resharpen with a file, and it leaves a ragged exit unless you back the workpiece.

Brad point bit
A twist drill reground for wood: a sharp central brad that pins the exact centre, plus two outer spurs that score the fibres before the lips lift the waste. It gives a clean-rimmed hole in timber, which a metal twist drill will not. Use it for dowel and shelf-pin holes.

Forstner bit
A flat-bottomed bit with a rim that cuts the circle first. It is the only common bit that will drill a flat-bottomed hole, an overlapping hole, or a clean hole on the edge of a board. Cabinet hinge cups in 26 and 35 mm are the classic use. It needs a drill press, not a hand drill, because the rim guides the cut and side loading ruins it.

Auger bit
A deep single or double helix with a threaded lead screw at the tip that pulls the bit into the timber and clears chips from deep holes. Used for joinery and for running cables and pipes through joists and beams. The lead screw means you must not use it in a high-speed drill.
Masonry bit
A steel body with a brazed tungsten carbide tip that is wider than the body, so the bit crushes rather than cuts. Run it in a hammer drill or rotary hammer at low speed with no water, and always remember that masonry bits are sized to the wall plug, not to the screw: a 6 mm plug wants a 6 mm bit. SDS shanks replace the plain round shank on rotary hammers.

Core drill
Three or four flutes and no cutting point at the centre, so it cannot start a hole from solid. Its job is to enlarge an existing cored or punched hole accurately, and the extra flutes give a better finish and truer hole than a twist drill can.
Gun drill
A single effective cutting edge with a V-shaped flute and an internal coolant channel. High-pressure coolant is pumped down the tool and flushes chips back along the flute, which is what makes depth-to-diameter ratios of 50:1 and more possible. Used for hydraulic cylinders, crankshaft oil galleries and mould cooling lines.
Hole saw
A cylindrical saw blade with a pilot drill at the centre. It cuts only the rim and leaves a disc, so it needs far less power than drilling out the whole area. Bimetal versions cut sheet steel and timber from about 14 to 150 mm, carbide grit versions cut tile.
Indexable insert drill
A steel body carrying two replaceable carbide inserts, one inboard and one outboard, with internal coolant holes. Used on CNC lathes and machining centres for large diameters from about 12 to 60 mm, where you swap a worn insert in a minute instead of regrinding a solid drill. It needs a very rigid setup and is not for a bench drill.
Drill bit materials and coatings
| Material | Hot hardness limit | Use it for |
|---|---|---|
| Carbon steel | Loses hardness around 200 degrees C | Wood and soft plastic only. Cheap, and it will not survive steel. |
| HSS (M2) | Holds hardness to roughly 550 degrees C | The workshop default. Mild steel, cast iron, aluminium, brass, plastic. |
| HSS-Co, M35 (5% cobalt) | Better red hardness and abrasion resistance than M2 | Stainless steel, cast iron and tougher alloy steels. The usual upgrade when plain HSS keeps burning out. |
| HSS-Co, M42 (8% cobalt) | Harder still, around 67 to 68 HRC | Hardened and heat-treated steels, titanium, Inconel. More brittle, so it needs a rigid machine. |
| Solid carbide | Stable well beyond 900 degrees C | Two to three times the cutting speed of HSS, and hardened steel up to about 60 HRC. Brittle, so it belongs on a CNC machine, not in a hand drill. |
Coatings are a few microns thick and add hardness and lubricity at the cutting edge:
- TiN (titanium nitride), the gold coloured one. Roughly 2300 HV, useful to about 600 degrees C. A general lift in tool life on steel and cast iron, and the cheapest upgrade available.
- TiCN (titanium carbonitride), blue-grey. Harder than TiN and better on abrasive material and cast iron, but less heat resistant.
- TiAlN / AlTiN (aluminium titanium nitride), violet to black. Forms an aluminium oxide skin at high temperature, so it works up to roughly 800 degrees C and is the coating for hard steel and dry or minimum-lubrication work. Not suited to aluminium, where it reacts and builds up on the edge.
- Black oxide is not a hard coating at all, just a surface treatment that resists rust and holds a little oil. It helps slightly on mild steel and nothing else.
A coating does not repair a bad grind. A sharp uncoated HSS drill beats a blunt coated one every time.
Drill bit sizes: the four size systems
Four different sizing systems are in daily use, and a drill index in an Indian workshop may carry two or three of them at once.
1. Metric sizes
Straightforward diameters in millimetres. Jobber series parallel shank drills under IS 5101 (aligned to ISO 235 and DIN 338) are normally stocked from 0.5 mm to 13 mm, in 0.1 mm or 0.5 mm steps depending on the set. Above 13 mm the drill usually moves to a Morse taper shank under IS 5103. Typical Indian sets are 1 to 10 mm in 0.5 mm steps (19 pieces) or 1 to 13 mm in 0.5 mm steps (25 pieces).
2. Fractional inch sizes
Steps of 1/64 inch (0.397 mm), from 1/16 inch upward. Common sizes and their metric equivalents: 1/8 in = 3.175 mm, 3/16 in = 4.763 mm, 1/4 in = 6.35 mm, 3/8 in = 9.525 mm, 1/2 in = 12.7 mm. Still common in India on older machines and for imperial threads.
3. Number gauge sizes
Wire gauge numbers running from #1 (5.791 mm, 0.2280 in) down to #80 (0.343 mm, 0.0135 in). The number gets larger as the drill gets smaller. These fill the gaps between fractional sizes and are the standard sizes quoted in imperial tap drill charts, for example a #7 drill for a 1/4-20 UNC tap.
4. Letter gauge sizes
Continues above #1, from A (5.944 mm, 0.234 in) to Z (10.49 mm, 0.413 in), getting larger as the letter advances. Used mostly for imperial tapping and reaming pilot sizes.
Tap drill size chart for metric coarse threads
This is the table most people come looking for. For ISO metric coarse threads the tap drill diameter is simply nominal diameter minus the pitch, which gives about 75 to 77 percent thread engagement. That is deliberate: a 75 percent thread carries close to full strength while taking far less tapping torque than a 100 percent thread, and chasing 100 percent is the fastest way to snap a small tap.
| Thread | Pitch (mm) | Tap drill (mm) | Clearance drill (mm) |
|---|---|---|---|
| M3 | 0.50 | 2.5 | 3.4 |
| M4 | 0.70 | 3.3 | 4.5 |
| M5 | 0.80 | 4.2 | 5.5 |
| M6 | 1.00 | 5.0 | 6.6 |
| M8 | 1.25 | 6.8 | 9.0 |
| M10 | 1.50 | 8.5 | 11.0 |
| M12 | 1.75 | 10.2 | 13.5 |
Check the arithmetic yourself: M12 gives 12 − 1.75 = 10.25 mm, and the nearest stocked drill is 10.2 mm. M8 gives 8 − 1.25 = 6.75, stocked as 6.8 mm. The clearance column is for the through hole in the top plate, where the bolt must pass freely rather than thread.
Fine pitch threads use the same rule with their own pitch, so M10 × 1.25 takes an 8.75 mm drill and M12 × 1.25 takes a 10.75 mm drill. Sizing a hole for a wall plug is different again: there the bit matches the plug diameter, not the screw.
Choosing and looking after drill bits
- Centre punch or spot drill before drilling anything that matters. The chisel edge will not self-centre unless the point is a split point.
- For holes above about 13 mm in steel, pilot drill first at roughly the web thickness of the final drill, then open out. This removes the chisel edge’s thrust load.
- Use cutting fluid on steel, soluble oil or neat cutting oil. Cast iron is normally drilled dry; aluminium likes kerosene or a dedicated aluminium cutting fluid.
- Resharpen at the first sign of a squeal or a blue chip. Keep both lips equal in length and equally angled about the axis, or the hole will come out oversize and the drill will wander.
- Store bits in an index, not loose in a drawer. Margins that knock against each other lose their guiding edge.
Drill bit selection follows the same logic as selecting any other piece of shop equipment: match the tool to the material and the duty, the way you would when choosing among the different types of pumps for a given fluid and head. The relevant syllabus context is set out in the AICTE Model Curriculum for Manufacturing Processes.
References
- ISO 5419:1982, Twist drills – Terms, definitions and types.
- ISO 235:2016, Parallel shank jobber and stub series drills and Morse taper shank drills.
- IS 5101, Twist drills, parallel shank, jobber series; IS 5102, long series; IS 5103, Morse taper shank. Bureau of Indian Standards.
- DIN 1836, tool types N, H and W for drilling tools.
FAQs
What are the main parts of a drill bit?
Shank, body, flutes, land with its margin, web, and the point. The point carries the two cutting lips, the chisel edge where the clearance faces meet, and the lip relief behind each edge. Taper shank drills add a tang that stops slip and lets a drift key remove the tool.
Which drill bit point angle should I use, 118 or 135 degrees?
Use 118 degrees for general work in mild steel, cast iron, brass and wood. Use a 135 degree split point for stainless steel, alloy steel and hardened material, and any time the surface is curved or slippery, because the split grind self-centres and will not walk.
What size drill bit is needed for an M8 tap?
6.8 mm. For ISO metric coarse threads the tap drill equals the nominal diameter minus the pitch, so M8 x 1.25 gives 8 – 1.25 = 6.75 mm, stocked as 6.8 mm. The same rule gives 2.5 mm for M3, 4.2 mm for M5, 5.0 mm for M6, 8.5 mm for M10 and 10.2 mm for M12.
What is the difference between HSS and cobalt drill bits?
Cobalt bits are HSS with 5 percent cobalt (M35) or 8 percent cobalt (M42) alloyed into the steel, which raises red hardness and abrasion resistance so the edge survives more heat. They cost more and are more brittle, and they are worth it for stainless steel, cast iron and hardened alloy steel rather than for ordinary mild steel.
Which standard covers twist drills?
ISO 5419 defines twist drill terms, definitions and types, and ISO 235 covers dimensions for parallel shank jobber and stub series drills and Morse taper shank drills. In India the corresponding Bureau of Indian Standards documents are IS 5101 for parallel shank jobber series, IS 5102 for long series and IS 5103 for Morse taper shank drills.