 EngineeringHulk
- Home
- Blog
- Manufacturing Engineering
- Brazing vs Soldering: Differences, Temperatures and When to Use Each
Brazing vs Soldering: Differences, Temperatures and When to Use Each
On this page
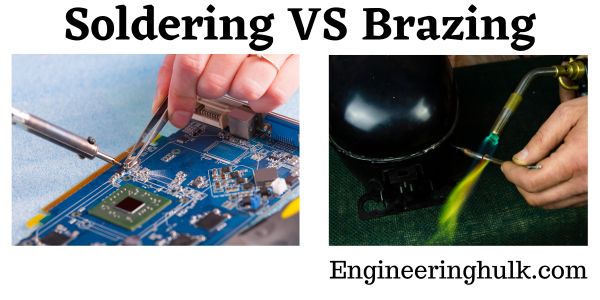
In both soldering and brazing only the filler metal melts; the base metal never does. The dividing line is the filler’s liquidus temperature: below 450 °C (840 °F) the process is soldering, above it the process is brazing. That is the American Welding Society definition in AWS A3.0, and it is the only real difference between the two. Everything else, from joint strength to heat source, follows from that temperature.
This page is the side-by-side comparison. For process steps see the separate pages on brazing and soldering.
Brazing vs soldering: comparison table
| Point | Soldering | Brazing |
|---|---|---|
| Filler liquidus | Below 450 °C (840 °F) | Above 450 °C (840 °F), but below the base metal’s solidus |
| Typical working temperature | About 180 to 350 °C | About 600 to 900 °C for torch work; up to about 1,150 °C for nickel alloys in a furnace |
| Filler alloys | Tin-lead (Sn63Pb37), lead-free tin-silver-copper (SAC305), tin-copper | Silver alloys (BAg), copper-phosphorus (BCuP), brass (copper-zinc), aluminium-silicon, nickel alloys |
| Joint strength | Low; the joint seals and conducts but should not carry structural load | High; a well-designed lap joint can be as strong as the parent metal |
| Joint clearance | About 0.10 to 0.15 mm on copper plumbing fittings | Typically 0.025 to 0.125 mm (0.001 to 0.005 in); strongest near 0.04 mm |
| Heat source | Soldering iron, hot air, reflow oven, wave machine, small gas torch for pipe | Oxy-fuel or air-fuel torch, induction coil, furnace (often vacuum or controlled atmosphere) |
| Flux | Rosin or no-clean flux for electronics; zinc chloride (acid) flux for plumbing and sheet metal | Borax and fluoride-based paste fluxes; none needed for copper-phosphorus on copper, or in vacuum and controlled-atmosphere furnaces |
| Typical uses | PCBs and wiring, copper water pipe, radiators, tin-plate, stained glass | AC and refrigeration copper lines, heat exchangers, carbide tool tips, bicycle frames, jewellery |
| Distortion | Negligible | Low, far less than welding, but the whole joint area gets red hot |
| Cost | Lowest: cheap tools and filler | Higher: torch gas and silver-bearing filler are expensive |
The differences explained
Why 450 °C?
The figure is a convention, not a physical boundary. AWS set it at 840 °F, which is 450 °C to the nearest round number, and ISO and the brazing industry use the same line. What matters is that it is measured on the filler’s liquidus, the temperature at which it is fully molten, not on the torch or the part. Any filler that is fully liquid below 450 °C is a solder, whatever the shop calls it.
Both depend on capillary action
Neither process melts the parent metal, so the filler has to be pulled into the joint. That is capillary action: molten filler wets clean metal and gets drawn into a narrow gap, even upwards against gravity. It only works when the gap is small and the surfaces are clean, which is why both processes need flux or a protective atmosphere, and why joint design is mostly about clearance.
Brazing is fussier about the gap. Research by the filler maker Lucas-Milhaupt found the strongest silver-brazed joint at a clearance of about 0.038 mm (0.0015 in), with joint strength dropping away on both sides. Too tight and the filler cannot enter; too wide and capillary pull is lost and the joint becomes a thick layer of weaker filler. Soldered copper plumbing works with a slightly wider gap, around 0.1 mm, because solder is so fluid and the joint is mainly a seal.
How strong is each joint?
Solder alloys are soft, low-melting metals, so the joint relies on large overlap and on the parts being held mechanically: a component lead through a PCB hole, or a pipe pushed fully into its socket. Brazing fillers are copper and silver alloys with much higher strength, and a brazed lap joint with an overlap of about three times the thinner wall is usually as strong as the tube itself. That is why pressurised refrigerant lines in air conditioners are brazed, not soldered.
Lead-free solders and RoHS
The traditional solder is Sn63Pb37, 63% tin and 37% lead, which melts sharply at 183 °C. The EU RoHS Directive (2011/65/EU) limits lead to 0.1% by weight in electrical and electronic equipment, with a few exemptions, and India’s E-Waste (Management) Rules carry similar limits. The standard replacement is SAC305: 96.5% tin, 3.0% silver and 0.5% copper, melting between 217 and 220 °C. That extra 35 °C or so is why lead-free work needs a hotter iron and why joints look duller. Drinking-water plumbing must use lead-free solder too.
Silver brazing alloys
Silver brazing fillers (the BAg family) are silver-copper-zinc alloys, often with tin, that flow at roughly 620 to 850 °C depending on silver content. More silver generally means a lower flow temperature, a more fluid filler and a higher price. They join steel, stainless, copper, brass and carbide to each other, which is their main advantage. Jewellers and plumbers often call this “silver soldering” or “hard soldering”, but because the filler liquidus is above 450 °C it is brazing by the AWS definition.
Brazing vs welding, briefly
Welding melts the base metal itself and fuses the parts, usually with a filler of matching composition. Brazing leaves the base metal solid. Welding gives the highest strength and handles thick sections and butt joints; brazing gives less distortion, joins dissimilar metals and thin walls, and makes many joints at once in a furnace. For welded joints see TIG welding.
When to use soldering vs brazing
- Solder electronics, wiring and anything heat-sensitive. A PCB, a plastic connector or a semiconductor will not survive brazing heat.
- Solder low-pressure copper water pipe and tin-plate where the joint only has to seal, and the service temperature stays well below about 100 °C.
- Braze joints under pressure or vibration: refrigeration and AC lines, gas lines, hydraulic fittings.
- Braze when the part runs hot. A solder joint softens long before its melting point, so it is not used near engines, burners or exhausts.
- Braze dissimilar metals such as copper to steel, or carbide tips to steel shanks, which cannot easily be welded.
- Weld, not braze, when the joint is thick, butt-jointed and carries the full structural load.
Common mistakes
- Heating the filler, not the joint. The parts must reach flow temperature so the filler melts on contact and wicks in. Melting filler with the flame or iron and dripping it on gives a cold, poorly bonded joint.
- Dirty surfaces. Flux removes light oxide, not grease, paint or heavy scale. Clean mechanically first.
- Wrong gap. A loose, oversized gap in brazing gives a weak, porous joint; a press fit leaves no room for the filler.
- Overheating. Burnt flux stops working, and overheated brazing filler can boil off zinc and leave porosity.
- Acid flux on electronics. Plumbing flux left on a circuit board keeps corroding it for months.
- Flux left on after brazing. Most brazing fluxes are corrosive; wash them off in hot water once the part has cooled.
- Calling silver brazing “soldering” and then picking a joint design, flux or heat source meant for soft solder.
References
- AWS A3.0M/A3.0, Standard Welding Terms and Definitions, definitions of brazing and soldering.
- AWS Brazing Handbook, recommended joint clearances by filler metal family.
- Directive 2011/65/EU on the restriction of hazardous substances in electrical and electronic equipment (RoHS).
- American Welding Society, brazing and soldering resources.
FAQs
What is the main difference between soldering and brazing?
The filler temperature. Soldering uses a filler with a liquidus below 450 °C (840 °F); brazing uses one above 450 °C but below the melting point of the base metal. In both, only the filler melts and it is drawn into the joint by capillary action. The higher temperature lets brazing use stronger copper and silver fillers.
Is brazing stronger than soldering?
Yes, by a wide margin. A soldered joint is mainly a seal or an electrical connection and should not carry structural load. A properly designed brazed lap joint, with the right clearance of about 0.025 to 0.125 mm, can be as strong as the parent metal.
Is silver soldering the same as brazing?
Usually, yes. Most “silver solder” used by jewellers and plumbers melts well above 450 °C, so under the AWS definition it is silver brazing. True soft solders containing silver, such as SAC305, melt at around 217 to 220 °C.
Can you braze with a soldering iron?
No. A soldering iron reaches roughly 300 to 450 °C at the tip and cannot heat a joint to the 600 °C and above that brazing fillers need. Brazing uses a gas torch, an induction coil or a furnace.
What is the difference between soldered and brazed copper pipe?
Soldered copper pipe uses a tin-based filler at about 200 to 250 °C and is used for water lines. Brazed copper pipe uses a copper-phosphorus or silver filler at 700 °C or more and gives a stronger joint that tolerates pressure, vibration and heat, which is why AC and refrigeration lines are brazed.
Related Topics on EngineeringHulk
Keep reading

Brazing Process: Joint Design, Filler Metals, Steps and Applications
What is brazing? Filler melting above 450 C is drawn into a tight joint by capillary action. Joint clearance, flux, heating methods, fillers and uses.
Soldering: Types, Process, Flux, Machines and Applications
Soldering explained: soft vs hard solder, 63/37 vs lead-free SAC305, flux types, iron temperature, PCB steps, wave vs reflow, defects and a reflow example.

What Is Annealing and How It Works: Stages, Types and Temperatures
Annealing softens metal by heating, soaking and slow cooling. See the three stages, recrystallisation temperature, steel annealing types and temperatures.
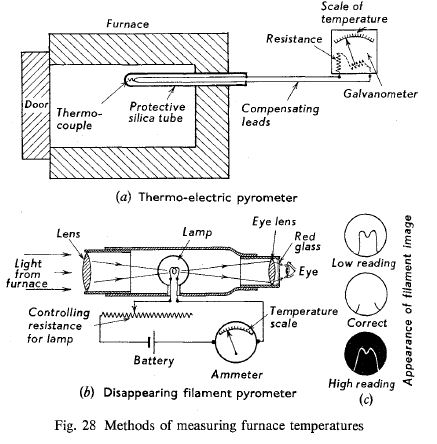
Heat Treatment of Steel: Processes, Temperatures, Cooling and Uses
Heat treatment of steel explained: annealing, normalising, hardening, tempering and case hardening, with temperatures, cooling media and a worked example.
The Evolution of Metal Machining in Automotive Manufacturing
How automotive machining evolved: manual tools, transfer lines, CNC, high-speed machining, near-net shape parts and EV-era changes like gigacasting.

Types of Tolerances in Engineering: Dimensional, Geometric and General
Types of tolerances explained: unilateral, bilateral and limit, GD&T form to runout, ISO 2768 classes, and a worked worst-case vs RSS stack-up example.